
 Deutsch
 English


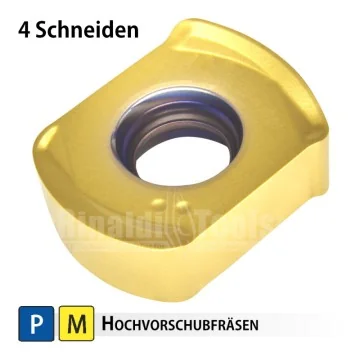

| Shape | LNMX |
| Processing | High Feed |
| Workpiece Material | Steel and Stainless Steel |
| Grade | RT330: PVD-coated P15-P25 and M10-M25 for universal use in steel and stainless steel |
| Cutting edges | 4 |
| Packaging unit | 10 Pc. |
| L | APmax | W | S | r | |
| LNMX 0904-MU RT330 | 11,94 | 1,50 | 9,2 | 4,79 | 1,20 |
.
| Item Nr. | L | APmax | W | S | r | |
| LNMX 0904-MU RT330 | 2301065 | 11,94 | 1,50 | 9,20 | 4,79 | 1,20 |
.
| Steel | Stainless Steel | |||
| Vc (m/min) | fz (mm) | Vc (m/min) | fz (mm) | |
| LNMX 0904-MU RT330 | 80-200 | 0,6-1,5 | 60-160 | 0,6-1,5 |
| Shape | LNMX |
| Processing | High Feed |
| Workpiece Material | Steel and Stainless Steel |
| Grade | RT330: PVD-coated P15-P25 and M10-M25 for universal use in steel and stainless steel |
| Cutting edges | 4 |
| Packaging unit | 10 Pc. |
| L | APmax | W | S | r | |
| LNMX 0904-MU RT330 | 11,94 | 1,50 | 9,2 | 4,79 | 1,20 |
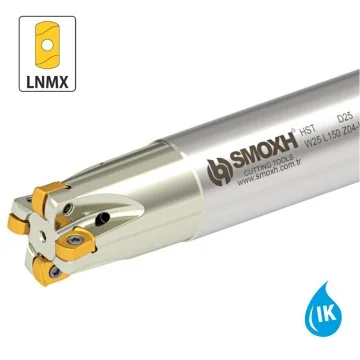
| Mill typ | High Feed Mill |
| Insert | LNMX 0904 |
| Packaging unit | 1 Pc. |
| D | d | L | L1 | Z | ap max | Insert | |
| HST BL09 D25 W25 L150 Z03-H | 25 | 25 | 150 | 40 | 3 | 1,5 | LNMX 0904 |
| HST BL09 D32 W32 L150 Z04-H | 32 | 32 | 150 | 40 | 4 | 1,5 | LNMX 0904 |
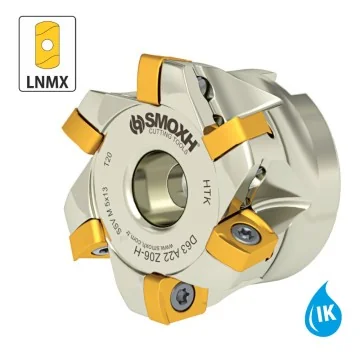
| Mill type | High Feed Mill |
| Insert | LNMX 0904 |
| Packaging unit | 1 Pc. |
| D | d | L | ap max | Z | Insert | |
| HTK BL09 D40 A16 Z05-H | 40 | 16 | 40 | 1,5 | 5 | LNMX 0904 |
| HTK BL09 D42 A16 Z05-H | 42 | 16 | 40 | 1,5 | 5 | LNMX 0904 |
| HTK BL09 D50 A22 Z06-H | 50 | 22 | 40 | 1,5 | 6 | LNMX 0904 |
| HTK BL09 D52 A22 Z06-H | 52 | 22 | 40 | 1,5 | 6 | LNMX 0904 |
| HTK BL09 D63 A22 Z07-H | 63 | 22 | 40 | 1,5 | 7 | LNMX 0904 |
| HTK BL09 D66 A27 Z08-H | 66 | 27 | 50 | 1,5 | 8 | LNMX 0904 |
| HTK BL09 D80 A27 Z10-H | 80 | 27 | 50 | 1,5 | 10 | LNMX 0904 |
| HTK BL09 D100 A32 Z12-H | 100 | 32 | 50 | 1,5 | 12 | LNMX 0904 |
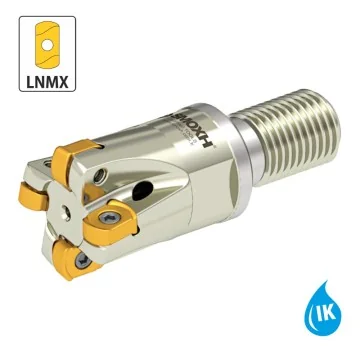
| Mill typ | High Feed Mill |
| Insert | LNMX 0904 |
| Packaging unit | 1 Pc. |
| D | Z | d1 | d2 | L | L1 | M | ap max | |
| MHT BL09 D25 M12 L35 Z03-H | 25 | 3 | 21 | 12,5 | 35 | 23 | 12 | 1,5 |
| MHT BL09 D32 M16 L43 Z04-H | 32 | 4 | 29 | 17 | 43 | 23 | 16 | 1,5 |
| MHT BL09 D35 M16 L43 Z04-H | 35 | 4 | 29 | 17 | 43 | 23 | 16 | 1,5 |
| MHT BL09 D40 M16 L43 Z05-H | 40 | 5 | 29 | 17 | 43 | 23 | 16 | 1,5 |

| Screw Type | Torx |
| Head Size | T10 |
| Torque | 2,9 Nm |
| Packaging unit | 1 piece |
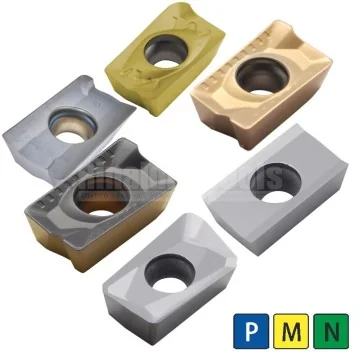
| Shape | APKT |
|
Grades |
RT400+: CVD-coated P30-P40 carbide for milling in steel |
| RT330: PVD-coated P15-P25 and M10-M25 for universal use in steel and stainless steel | |
| RT300: PVD-coated P15-P25 and M10-M25 for universal use in steel and stainless steel | |
| RT100: Uncoated K10-K15 carbide for ALU and plastics | |
| Packaging unit | 10 Pc. |
| L | d | s | d1 | r | |
| APKT 1604PDSR-30 RT400+ | 16,50 | 9,54 | 4,76 | 4,4 | 0,8 |
| APKT 1604PDSR-30 RT330 | 16,50 | 9,54 | 4,76 | 4,4 | 0,8 |
| APKT 1604PDTR RT300 | 16,50 | 9,54 | 4,76 | 4,4 | 0,95 |
| APKT 160424PDTR RT330 | 16,50 | 9,54 | 4,76 | 4,4 | 2,4 |
| APKT 1604-ALZ RT100 | 16,50 | 9,54 | 4,76 | 4,4 | 0,4 |
| APKT 160408-AL RT100 | 16,50 | 9,54 | 4,76 | 4,4 | 0,8 |

| Shape | LNKT |
| Workpiece Material | Cast Iron |
| Grade | RT150K: CVD-coated K10-K20 carbide for cast machining |
| Packaging unit | 10 Pc. |
| L | S | W | r | |
| LNKT 080408-GM RT150K | 8,75 | 4,45 | 8,75 | 0,8 |
| LNKT 120608-GM RT150K | 12,7 | 6,75 | 12,7 | 0,8 |
| LNKT 160708-GM RT150K | 16,05 | 7,35 | 16,05 | 0,8 |

| Shape | RTHX |
| Workpiece Material | Steel and Stainless Steel |
| Processing | Medium |
| Grade | RT350: PVD-coated carbide for finishing and medium machining across a wide range of applications |
| MOQ | 2 Pc. |
- Highly stable cutting edge due to 0° rake angle with defined clearance angle
| r | I.C. | S | d | |
| RTHX 1203-GM RT350 | 6 | 12 | 3 | 4 |
| RTHX 1604-GM RT350 | 8 | 16 | 4 | 5 |
| RTHX 2005-GM RT350 | 10 | 20 | 5 | 5 |
| RTHX 2506-GM RT350 | 12,5 | 25 | 6 | 6 |
| RTHX 3007-GM RT350 | 15 | 30 | 7 | 8 |
| RTHX 3207-GM RT350 | 16 | 32 | 7 | 8 |
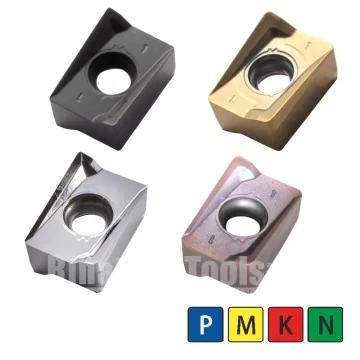
| Shape | ANGX |
|
Grades |
RT150K: CVD-coated K10-K20 carbide for casting machining |
| RT250X: PVD multilayer coated P10-P30 and M10-M30 carbide for universal use in steel and stainless steel | |
| RT100: uncoated K10-K20 carbide for casting machining | |
| RT305H: PVD-coated high-performance grade for a wide range of applications. | |
| Packaging unit | 10 Pc. |
| L | S | d | W | r | ap max | |
| ANGX 110508-GM RT150K | 11,85 | 5,7 | 3,5 | 8,4 | 0,8 | 11,2 |
| ANGX 110508-GM RT250X | 11,85 | 5,7 | 3,5 | 8,4 | 0,8 | 11,2 |
| ANGX 110504-ALZ RT100 | 11,85 | 5,7 | 3,5 | 8,4 | 0,4 | 11,2 |
| ANGX 110508-GM RT305H | 11,85 | 5,7 | 3,5 | 8,4 | 0,8 | 11,2 |
| ANGX 110520-GM RT305H | 11,85 | 5,7 | 3,5 | 8,4 | 2,0 | 11,2 |
| L | S | d | W | r | ap max | |
| ANGX 150608-GM RT150K | 15,43 | 7,3 | 4,4 | 11 | 0,8 | 14,5 |
| ANGX 150608-GM RT250X | 15,43 | 7,3 | 4,4 | 11 | 0,8 | 14,5 |
| ANGX 150608-ALZ RT100 | 15,43 | 7,3 | 4,4 | 11 | 0,8 | 14,5 |
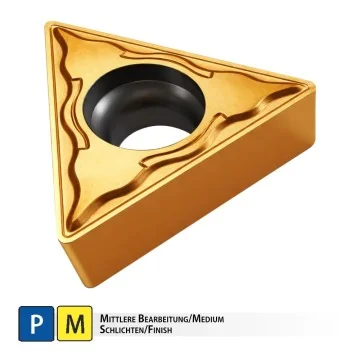
| Shape | TCMT |
| Processing | Medium and finish |
| Cutting conditions | Continuous and light interrupted |
| Workpiece Material | Steel and Stainless Steel |
| Grade | RT250X: PVD multilayer coated P10-P30 and M10-M30 carbide for universal use in steel and stainless steel |
| Packaging unit | 10 Pc. |
| r | L | I.C | S | d | |
| TCMT 110204-HF RT250X | 0,4 | 11 | 6,35 | 2,38 | 2,8 |
| TCMT 110208-HF RT250X | 0,8 | 11 | 6,35 | 2,38 | 2,8 |
| TCMT 16T304-HF RT250X | 0,4 | 16,5 | 9,525 | 3,97 | 4,4 |
| TCMT 16T308-HF RT250X | 0,8 | 16,5 | 9,525 | 3,97 | 4,4 |

| Shape | SEET |
| Grades | RT100: Uncoated K10-K15 carbide for aluminum and plastics |
| RT150K: CVD-coated K10-K20 carbide for cast iron machining | |
| RT250X: PVD-Multilayer Beschichtetes P10-P30 und M10-M30 Hartmetall für die Universelle Anwendung in Stahl und Edelstahl | |
| RT300: PVD-coated P15-P25 and M10-M25 for universal use in steel and stainless steel | |
| RTC: RTC-Uncoated cermet grade for precision machining in steel and stainless steel | |
| RT300P: CVD-coated P25-P35-TIN carbide for roughing in steel and in interrupted cuts | |
| RT400P: PVD-coated P40 carbide grade for rough steel machining | |
| RT350M: CVD-coated M20-M35 carbide for milling in stainless steel | |
| Packagig Unit | 10 pc. |
| L | I.C | S | d | |
| SEET 12T3-DM RT250X | 13,4 | 13,4 | 3,97 | 4,1 |
| SEET 12T3-PM RT300 | 13,4 | 13,4 | 3,97 | 4,1 |
| SEET 12T3-DF RTC | 13,4 | 13,4 | 3,97 | 4,1 |
| SEET 12T3-DM RT300P | 13,4 | 13,4 | 3,97 | 4,1 |
| SEET 12T3-DM RT400P | 13,4 | 13,4 | 3,97 | 4,1 |
| SEET 12T3-EM RT350M | 13,4 | 13,4 | 3,97 | 4,1 |
| SEET 12T3-ALZ RT100 | 13,4 | 13,4 | 3,97 | 4,1 |
| SEET 12T3-DM RT150K | 13,4 | 13,4 | 3,97 | 4,1 |

| Shape | RDKW |
| Processing | Medium |
| Workpiece Material | Steel and Cast Iron |
| Grade | RT300: PVD-coated P15-P25 and M10-M25 for universal use in steel and stainless steel |
| Packaging unit | 10 Pc. |
| I.C | S | d | |
| RDKW 0803MO RT300 | 8 | 3,18 | 3,4 |
| RDKW 10T3MO RT300 | 10 | 3,97 | 4,1 |
| RDKW 1204MO RT300 | 12 | 4,76 | 4,4 |
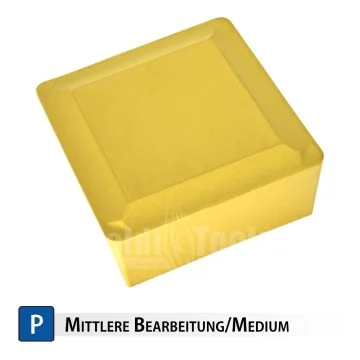
| Shape | SPMR |
| Processing | Medium |
| Workpiece Material | Steel |
| Grade | RT250: CVD-coated P25-TIN hard metal for general steel processing |
| Packaging unit | 10 Pc. |
| r | L | I.C. | S | |
| SPMR 120308-PM RT250 | 0,8 | 12,7 | 12,7 | 3,18 |

| Shape | RDKW |
| Processing | Medium |
| Workpiece Material | Hard Materials |
| Grade | RT105H: PVD-TiALN coated M10-M20 carbide for hard materials |
| Packaging unit | 10 Pc. |
| I.C | S | d | |
| RDKW 0702MO RT105H HART | 7 | 2,38 | 2,7 |
| RDKW 1003MO RT105H HART | 10 | 3,18 | 3,9 |
| RDKW 10T3MO RT105H HART | 10 | 3,97 | 4,4 |
| RDKW 12T3MO RT105H HART | 12 | 3,97 | 3,9 |
| RDKW 1204MO RT105H HART | 12 | 4,76 | 4,4 |
| RDKW 1604MO RT105H HART | 16 | 4,76 | 5,2 |

| Shape | RDKW |
| Processing | Medium |
| Workpiece Material | Steel and Cast Iron |
| Grade | RT300: PVD-coated P15-P25 and M10-M25 for universal use in steel and stainless steel |
| Packaging unit | 10 Pc. |
| I.C | S | d | |
| RDKW 0702MO RT300 | 7 | 2,38 | 2,7 |
| RDKW 1003MO RT300 | 10 | 3,18 | 3,9 |
| RDKW 12T3MO RT300 | 12 | 3,97 | 3,9 |
| RDKW 1604MO RT300 | 16 | 4,76 | 5,2 |

| Grooving Insert | RT22R/L RT305 |
| Workpiece Materials | Steel and Stainless Steel |
| Grooving system | RT-System |
| Grade | RT305 = PVD grade M20-M30 for stainless steel with the most modern coating |
| Packaging unit | 5 Pc. |
| W±0,025 | r | La max | øI.C | S | |
| RT22L100-R02 RT305 | 1,0 | 0,2 | 2 | 12,7 | 4,76 |
| RT22R125-R02 RT305 | 1,25 | 0,2 | 2 | 12,7 | 4,76 |
| RT22L125-R02 RT305 | 1,25 | 0,2 | 2 | 12,7 | 4,76 |
| RT22R145-R02 RT305 | 1,45 | 0,2 | 2 | 12,7 | 4,76 |
| RT22L145-R02 RT305 | 1,45 | 0,2 | 2 | 12,7 | 4,76 |
| RT22R150-R02 RT305 | 1,5 | 0,2 | 3,5 | 12,7 | 4,76 |
| RT22L150-R02 RT305 | 1,5 | 0,2 | 3,5 | 12,7 | 4,76 |
| RT22R175-R02 RT305 | 1,75 | 0,2 | 3,5 | 12,7 | 4,76 |
| RT22L175-R02 RT305 | 1,75 | 0,2 | 3,5 | 12,7 | 4,76 |
| RT22R185-R02 RT305 | 1,85 | 0,2 | 3,5 | 12,7 | 4,76 |
| RT22L185-R02 RT305 | 1,85 | 0,2 | 3,5 | 12,7 | 4,76 |
| RT22R195-R02 RT305 | 1,95 | 0,2 | 3,5 | 12,7 | 4,76 |
| RT22R200-R02 RT305 | 2,0 | 0,2 | 3,5 | 12,7 | 4,76 |
| RT22L200-R02 RT305 | 2,0 | 0,2 | 3,5 | 12,7 | 4,76 |
| RT22R225-R02 RT305 | 2,25 | 0,2 | 3,5 | 12,7 | 4,76 |
| RT22R230-R02 RT305 | 2,3 | 0,2 | 3,5 | 12,7 | 4,76 |
| RT22L230-R02 RT305 | 2,3 | 0,2 | 3,5 | 12,7 | 4,76 |
| RT22R250-R03 RT305 | 2,5 | 0,3 | 4 | 12,7 | 4,76 |
| RT22L250-R03 RT305 | 2,5 | 0,3 | 4 | 12,7 | 4,76 |
| RT22R265-R03 RT305 | 2,65 | 0,3 | 4 | 12,7 | 4,76 |
| RT22L265-R03 RT305 | 2,65 | 0,3 | 4 | 12,7 | 4,76 |
| RT22R280-R03 RT305 | 2,8 | 0,3 | 4 | 12,7 | 4,76 |
| RT22L280-R03 RT305 | 2,8 | 0,3 | 4 | 12,7 | 4,76 |
| RT22R300-R03 RT305 | 3,0 | 0,3 | 4 | 12,7 | 4,76 |
| RT22L300-R03 RT305 | 3,0 | 0,3 | 4 | 12,7 | 4,76 |
| RT22R320-R03 RT305 | 3,2 | 0,3 | 4 | 12,7 | 4,76 |
| RT22L320-R03 RT305 | 3,2 | 0,3 | 4 | 12,7 | 4,76 |
| RT22R330-R03 RT305 | 3,3 | 0,3 | 4 | 12,7 | 4,76 |
| RT22L330-R03 RT305 | 3,3 | 0,3 | 4 | 12,7 | 4,76 |
| RT22R350-R03 RT305 | 3,5 | 0,3 | 5 | 12,7 | 4,76 |
| RT22L350-R03 RT305 | 3,5 | 0,3 | 5 | 12,7 | 4,76 |
| RT22R400-R04 RT305 | 4,0 | 0,4 | 5 | 12,7 | 4,76 |
| RT22L400-R04 RT305 | 4,0 | 0,4 | 5 | 12,7 | 4,76 |
| RT22R430-R04 RT305 | 4,3 | 0,4 | 5 | 12,7 | 4,76 |
| RT22L430-R04 RT305 | 4,3 | 0,4 | 5 | 12,7 | 4,76 |
| RT22R450-R04 RT305 | 4,5 | 0,4 | 5 | 12,7 | 4,76 |
| RT22L450-R04 RT305 | 4,5 | 0,4 | 5 | 12,7 | 4,76 |
| RT22R480-R04 RT305 | 4,8 | 0,4 | 5 | 12,7 | 5,06 |
| RT22L480-R04 RT305 | 4,8 | 0,4 | 5 | 12,7 | 5,06 |
The RT22R/L RT305 grooving insert is a high-performance component for the RT grooving system, designed for the reliable machining of steel and stainless steel. Featuring the modern PVD coating of grade M20-M30, it supports efficient workflows in parting and grooving operations. The combination of wear-resistant cutting material and a robust edge design provides professional users with high process stability on both CNC and conventional lathes.

| Shape | ONHU |
| Workpiece Materials |
RT250X: Steel and Stainless Steel RT150K: Cast Iron |
| Grades |
RT250X: PVD multilayer coated P10-P30 and M10-M30 carbide for universal use in steel and stainless steel |
|
RT150K: CVD-coated K10-K20 carbide for rough cast machining |
|
| Packaging unit | 10 Pc. |
| r | L | I.C. | S | d | Scope of Application | |
| ONHU 060408-GM RT250X | 0,8 | 6,15 | 15,8 | 5,54 | 6,02 | Steel & Stainless Steel |
| ONHU 060408-GM RT150K | 0,8 | 6,15 | 15,8 | 5,54 | 6,02 | Cast Iron |

| Shape | RTHX |
| Workpiece Material | Steel and Stainless Steel |
| Processing | Finishing and Precision-Finishing |
| Grade | RT350: PVD-coated carbide for finishing and medium machining across a wide range of applications |
| MOQ | 2 Pc. |
- Sharp and stable cutting edge design featuring a positive rake angle and double clearance angle
- Particularly suitable for high-precision and finishing operations under stable machine conditions
| r | I.C. | S | d | |
| RTHX 1203-GF RT350 | 6 | 12 | 3 | 4 |
| RTHX 1604-GF RT350 | 8 | 16 | 4 | 5 |
| RTHX 2005-GF RT350 | 10 | 20 | 5 | 5 |
| RTHX 2506-GF RT350 | 12,5 | 25 | 6 | 6 |
| RTHX 3007-GF RT350 | 15 | 30 | 7 | 8 |
| RTHX 3207-GF RT350 | 16 | 32 | 7 | 8 |
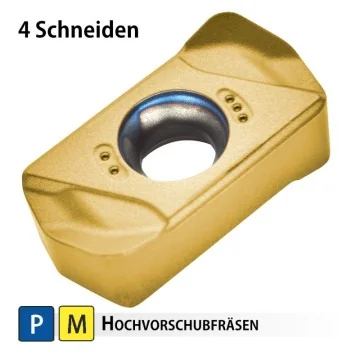
| Shape | LNMX |
| Processing | High Feed |
| Workpiece Material | Steel and Stainless Steel |
| Grade |
RT300: PVD-coated P15-P25 and M10-M25 for universal use in steel and stainless steel |
|
RT330: PVD-coated P15-P25 and M10-M25 with additional TiN-coating for improved wear-detection |
|
| Packaging unit | 10 Pc. |
.
| L | apmax | W | S | r | |
| LNMX 0303-MU RT300 | 11,86 | 1,00 | 6 | 4,29 | 1,20 |
| LNMX 0303-MU RT330 New! | 11,86 | 1,00 | 6 | 4,29 | 1,20 |
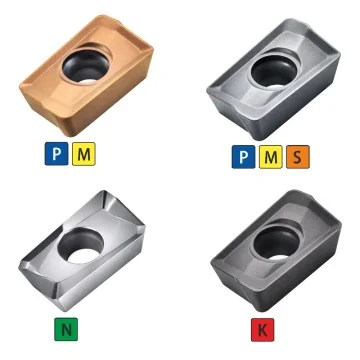
| Shape | APKT |
|
Grades |
RT250X = PVD multilayer coated P10-P30 and M10-M30 carbide for universal use in steel and stainless steel |
| RT250K = CVD-coated K10-K20 carbide for rough cast machining | |
| RT100 = Uncoated K10-K15 carbide for ALU and plastics | |
| RT305H: PVD-coated high-performance grade for a wide range of applications. | |
| Packaging unit | 10 Pc. |
| L | d | s | I.W | r | |
| APKT 11T304-PF RT250X | 12,24 | 2,8 | 3,6 | 6,5 | 0,4 |
| APKT 11T308-PM RT250X | 12,24 | 2,8 | 3,6 | 6,5 | 0,8 |
| APKT 11T312-PM RT250X | 12,24 | 2,8 | 3,6 | 6,5 | 1,2 |
| APKT 11T316-PM RT250X | 12,24 | 2,8 | 3,6 | 6,5 | 1,6 |
| APKT 11T320-PM RT250X | 12,24 | 2,8 | 3,6 | 6,5 | 2,0 |
| APKT 11T304-PM RT150K | 12,24 | 2,8 | 3,6 | 6,5 | 0,4 |
| APKT 11T308-PM RT150K | 12,24 | 2,8 | 3,6 | 6,5 | 0,8 |
| APKT 11T312-PM RT150K | 12,24 | 2,8 | 3,6 | 6,5 | 1,2 |
| APKT 11T316-PM RT150K | 12,24 | 2,8 | 3,6 | 6,5 | 1,6 |
| APKT 11T320-PM RT150K | 12,24 | 2,8 | 3,6 | 6,5 | 2,0 |
| APKT 11T304-ALZ RT100 | 12,24 | 2,8 | 3,6 | 6,5 | 0,4 |
| APKT 11T308-ALZ RT100 | 12,24 | 2,8 | 3,6 | 6,5 | 0,8 |
| APKT 11T308-PM RT305H | 12,24 | 2,8 | 3,6 | 6,5 | 0,8 |
| APKT 11T316-PM RT305H | 12,24 | 2,8 | 3,6 | 6,5 | 1,6 |
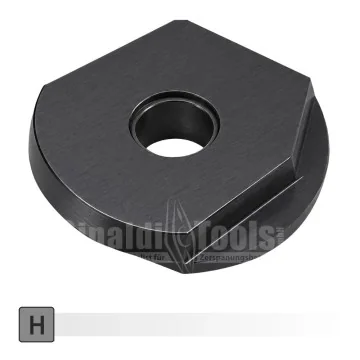
| Shape | RTHX |
| Workpiece Material | Hardened Steel up to 68 HRC |
| Processing | Finishing |
| Grade | RT350: PVD-coated carbide for high-performance machining of hardened steel |
| MOQ | 10 Pc. |
- Highly wear-resistant substrate for long tool life when machining hardened Steel
- Special TiAlN coating reduces built-up edge formation and improves surface finish
| r | I.C. | S | d | |
| RTHX 1203-HM RT905H | 6 | 12 | 3 | 4 |
| RTHX 1604-HM RT905H | 8 | 16 | 4 | 5 |
| RTHX 2005-HM RT905H | 10 | 20 | 5 | 5 |
| RTHX 2506-HM RT905H | 12,5 | 25 | 6 | 6 |
| RTHX 3007-HM RT905H | 15 | 30 | 7 | 8 |
| RTHX 3207-HM RT905H | 16 | 32 | 7 | 8 |