
 Deutsch
 English
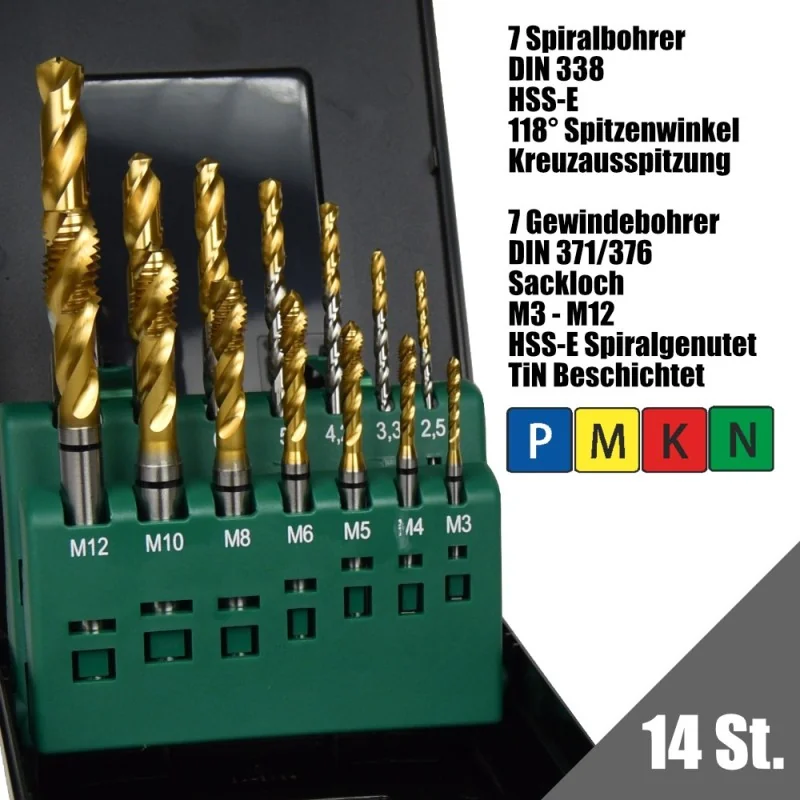




| Tap Typ | HSS-E-TiN |
| Hole | Blind Hole |
| Thread | Metric |
| Length | Jobber |
| Materials | Steel, Stainless Steel, Cast Iron and NF-Materials |
| Flank Angle | 60° |
| Packaging unit | 1 Pc. |
This precisely matched machining set provides professional users with a high-performance complete solution for generating metric internal threads in blind holes. The premium HSS-E tools with wear-resistant TiN coating ensure reliable results in steel, stainless steel, and cast iron, while the included core hole drills allow for immediate use without time-consuming tool changes.
The Set HSS-E-Tap Blind hole, metric 60° is a well-thought-out complete solution for machinists requiring a dependable basis for manufacturing accurate threads. By combining precisely coordinated twist drills and machine taps, this tool arrangement consistently supports efficient workflows. It enables the economical and process-reliable production of metric internal threads in blind holes while minimizing setup times.
| Tap | D | P | L2 | L | L4 | d | K | Kl | Z |
| 1x GB-S-ISO-M3-HSS-E-TIN | M3 | 0,5 | 6 | 56 | 18 | 3,5 | 2,7 | 6 | 3 |
| 1x GB-S-ISO-M4-HSS-E-TIN | M4 | 0,7 | 7 | 63 | 21 | 4,5 | 3,4 | 6 | 3 |
| 1x GB-S-ISO-M5-HSS-E-TIN | M5 | 0,8 | 8 | 70 | 25 | 6 | 4,9 | 8 | 3 |
| 1x GB-S-ISO-M6-HSS-E-TIN | M6 | 1 | 10 | 80 | 30 | 6 | 4,9 | 8 | 3 |
| 1x GB-S-ISO-M8-HSS-E-TIN | M8 | 1,25 | 13 | 90 | 35 | 8 | 6,2 | 9 | 3 |
| 1x GB-S-ISO-M10-HSS-E-TIN | M10 | 1,5 | 15 | 100 | 39 | 10 | 8 | 11 | 3 |
| 1x GB-S-ISO-M12-HSS-E-TIN | M12 | 1,75 | 18 | 110 | 44 | 9 | 7 | 10 | 3 |
| Core Hole Drill | Thread | D | L1 | L |
| 1x SB-D2,5-J-HSS-E-TIN |
M3 | 2,5 | 30 | 57 |
| 1x SB-D3,3-J-HSS-E-TIN |
M4 | 3,3 | 36 | 65 |
| 1x SB-D4,2-J-HSS-E-TIN |
M5 | 4,2 | 43 | 75 |
| 1x SB-D5,0-J-HSS-E-TIN |
M6 | 5,0 | 52 | 86 |
| 1x SB-D6,8-J-HSS-E-TIN |
M8 | 6,8 | 69 | 109 |
| 1x SB-D8,5-J-HSS-E-TIN |
M10 | 8,5 | 75 | 117 |
| 1x SB-D10,2-J-HSS-E-TIN |
M12 | 10,2 | 87 | 133 |
| Workpiece Material | Tensile strength | Cutting Speed |
| (N/mm²) | Vc (m/min) | |
| Structural Steel | <450 | 10-25 |
| Tempered Steel | 450-700 | 5-20 |
| Tooling Steel | >700 | 5-7 |
| Stainless Steel | <1100 | 6-15 |
| Cast Iron | 8-20 | |
| Aluminum cast alloys (<12% Si.) | <600 | 20-25 |
| Copper/Brass | <850 | 12-40 |
| Workpiece Material | Tensile strength | Cutting Speed | Feed (mm) | ||
| (N/mm²) | Vc (m/min) | Ø 2-4 | Ø 6-8 | Ø 10-13 | |
| Structural Steel | <450 | 15-28 | 0,04-0,12 | 0,12-0,18 | 0,16-0,24 |
| Tempered Steel | 450-700 | 20-25 | 0,04-0,12 | 0,12-0,18 | 0,16-0,24 |
| Tooling Steel | >700 | 15 | 0,04-0,08 | 0,12-0,18 | 0,16-0,24 |
| Stainless Steel | <1100 | 10-18 | 0,04-0,12 | 0,12-0,18 | 0,16-0,24 |
| Cast Iron | 20-28 | 0,04-0,12 | 0,04-0,18 | 0,08-0,24 | |
| Aluminum cast alloys (<12% Si.) | <600 | 35-45 | 0,04-0,16 | 0,12-0,2 | 0,16-0,28 |
| Copper/Brass | <850 | 20-35 | 0,05-0,16 | 0,12-0,18 | 0,053 |
This carefully assembled set creates excellent conditions for demanding drilling and thread cutting processes in modern mechanical engineering and plant construction. It is designed for machining structural steel, tempered steel, stainless steel, cast iron, as well as non-ferrous metals like aluminum and brass. The universal Jobber length of the tools opens up flexible application possibilities on manual drilling and turning machines, as well as on high-performance CNC machining centers.
The HSS-E drills and taps are equipped with a high-quality titanium nitride (TiN) coating, which contributes to increased thermal load capacity and high wear resistance. Since the assortment bundles all necessary core hole and blind hole taps into one package, the time-consuming search for individual tools is eliminated. In addition, the precisely ground 60° flank angle ensures an accurate geometry of the generated internal threads, supporting secure assembly and high load-bearing capacity of the component connections.
| Tap Typ | HSS-E-TiN |
| Hole | Blind Hole |
| Thread | Metric |
| Length | Jobber |
| Materials | Steel, Stainless Steel, Cast Iron and NF-Materials |
| Flank Angle | 60° |
| Packaging unit | 1 Pc. |
This precisely matched machining set provides professional users with a high-performance complete solution for generating metric internal threads in blind holes. The premium HSS-E tools with wear-resistant TiN coating ensure reliable results in steel, stainless steel, and cast iron, while the included core hole drills allow for immediate use without time-consuming tool changes.
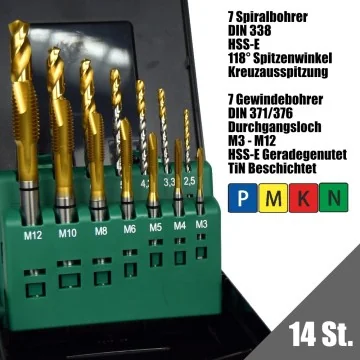
| Tap Typ | HSS-E-TiN |
| Hole | Trough Hole |
| Thread | Metric |
| Length | Jobber |
| Materials | Steel, Stainless Steel, Cast Iron and NF-Materials |
| Flank Angle | 60° |
| Packaging unit | 1 Pc. |
This complete set of HSS-E taps and perfectly matched core hole drills provides a practical solution for producing metric internal threads. Specifically designed for through holes, the TiN-coated tools support efficient and consistent machining processes in professional metalworking.

| d | H | L | f | Dmin | |
| S08H SCLCR/L 06 | 8 | 7 | 100 | 07 | ≥11 |
| S10K SCLCR/L 06 | 10 | 9 | 125 | 08 | ≥13 |
| S12K SCLCR/L 06 | 12 | 11 | 125 | 10 | ≥16 |
| S16P SCLCR/L 09 | 16 | 15 | 170 | 13 | ≥21 |
The four-piece S-SCLCR/L (95°) set from SMOXH offers a well-thought-out tool selection for professional internal turning applications. Available in right-hand or left-hand versions, these boring bars cover a broad spectrum of inner contours with diameters from 8 to 16 mm, creating excellent conditions for stable machining processes.
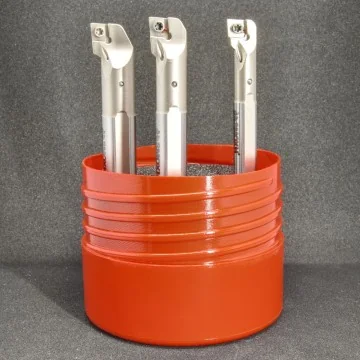
| Boring Bar | SCLCR/L |
| Cutting Angle | 95° |
| Insert | CC.. |
| Main application | Longitudinal turning, Facing |
| Clamping | Screw Clamping |
| Cooling | Without Cooling Holes |
| Packaging unit | 1 Pc. |
| d | H | L | f | Dmin | |
| 1x A08H SCLCR/L 06 | 8 | 7 | 100 | 07 | ≥11 |
| 1x A10H SCLCR/L 06 | 10 | 9 | 100 | 08 | ≥13 |
| 1x A12H SCLCR/L 06 | 12 | 11 | 100 | 10 | ≥16 |
The three-piece A-Boring Bars-Set SCLCR/L is consistently tailored for professional use in internal longitudinal turning and facing operations. Featuring a 95° approach angle and a robust screw clamping mechanism, this holder system establishes good conditions for stable and precise machining processes.
| d | H | L | f | Dmin | |
| A10H SDQCR/L-07 with cooling holes | 10 | 09 | 100 | 08 | ≥13 |
| A12H SDQCR/L-07 with cooling holes | 12 | 11 | 100 | 10 | ≥16 |
| A16M SDQCR/L-11 with cooling holes | 16 | 15 | 150 | 13 | ≥21 |
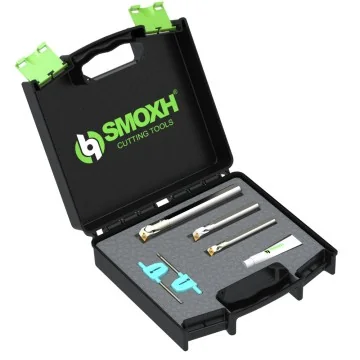
The A-SDQCR/L (107.5°) Set Inside turning holders with cooling holes by SMOXH is designed for precise and demanding internal machining. The set consists of the right version (Art. Nr. Right: SM59917) and the left version (Art. Nr. Left: SM59924). Featuring a robust steel shank and internal coolant supply, it supports efficient chip evacuation. Packaging Unit = 1 Pc.
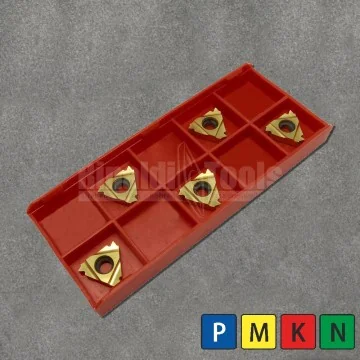
The Set 2 - 16IR-V-... RT330 (Universal) contains five high-quality internal threading inserts with a full profile geometry for metric ISO threads. This practical combination provides professional users with the right pitches for common thread turning operations, featuring a versatile universal grade.
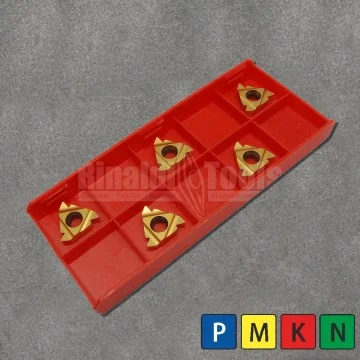
The Set 3 - 16ER-V-... RT330 (Universal) combines five standard metric ISO threading inserts of size 16ER in a convenient package. With pitches ranging from 1.0 to 2.0 mm and the universal RT330 coating, professional users receive a well-thought-out solution for flexible turning applications.
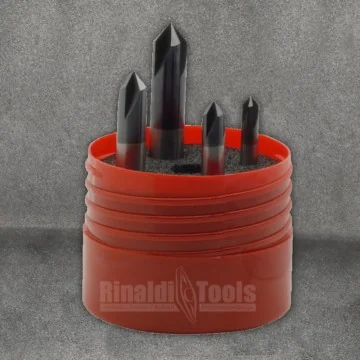
| d(h6) | L | D | Shank | X | Z | |
| 6 | 6 | 55 | 0,2 | HB | 90 | 4 |
| 8 | 8 | 58 | 0,5 | HB | 90 | 4 |
| 10 | 10 | 65 | 0,5 | HB | 90 | 4 |
| 12 | 12 | 75 | 0,5 | HB | 90 | 4 |
The four-piece Solid Carbide Chamfer Mills Set 90° provides the ideal tools for clean chamfering and deburring of workpiece edges. The solid carbide construction with an h6 tolerance cylindrical shank and four flutes ensures high process reliability and uniform chamfer widths across various machining tasks.
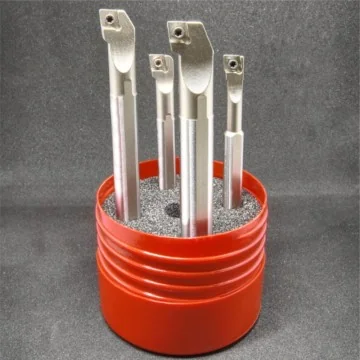
| Boring Bar | SCLCR/L |
| Cutting Angle | 95° |
| Insert | CC.. |
| Main application | Longitudinal turning, Facing |
| Clamping | Screw Clamping |
| Cooling | Without Cooling Holes |
| Packaging unit | 1 Pc. |
| d | H | L | f | Dmin | |
| 1x S0608H SCLCR/L 06 | 8 | 7 | 100 | 05 | ≥8 Neck Diameter 6mm |
| 1x S08H SCLCR/L 06 | 8 | 7 | 100 | 07 | ≥11 |
| 1x S10K SCLCR/L 06 | 10 | 9 | 125 | 08 | ≥13 |
| 1x S12K SCLCR/L 06 | 12 | 11 | 125 | 10 | ≥16 |
This versatile S-Boring Bars-Set offers a well-thought-out selection of boring bars for precise longitudinal turning and facing. Featuring shank diameters from 8 mm to 12 mm and a 95° cutting angle, this 4-piece kit enables flexible operations in modern metalworking tasks.
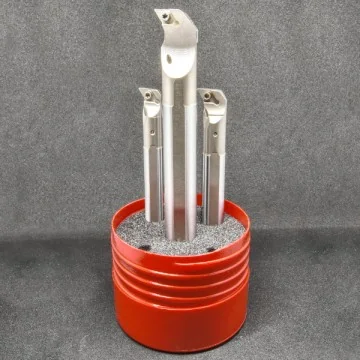
| Boring Bar | SDUCR/L |
| Cutting Angle | 93° |
| Insert | DC.. |
| Clamping | Screw Clamping |
| Cooling | With Cooling Holes |
| Packaging unit | 1 Pc. |
| d | h | L | f | Dmin | |
| 1x A10H SDUCR/L-07 mit IK | 12 | 11 | 100 | 10 | ≥13 |
| 1x A12H SDUCR/L-07 mit IK | 12 | 11 | 100 | 10 | ≥16 |
| 1x A16M SDUCR/L-07 mit IK | 16 | 15 | 150 | 13 | ≥21 |
The 3-piece A-Boring Bars-Set SDUCR/L with cooling holes is designed for demanding internal turning and contouring applications. With a 93° approach angle and compatibility with DC indexable inserts, this tool holder system offers versatile options for various bore diameters.
| d | H | L | f | Dmin | |
| S10K SDUCR/L 07 | 10 | 9 | 125 | 08 | ≥13 |
| S12K SDUCR/L 07 | 12 | 11 | 125 | 10 | ≥16 |
| S16P SDUCR/L 11 | 16 | 15 | 170 | 13 | ≥21 |
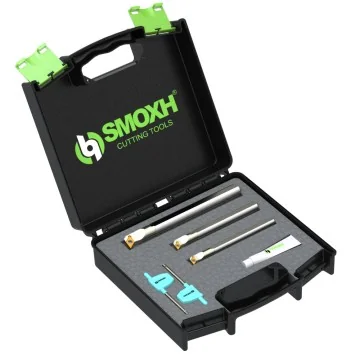
The S-SDUCR/L (93°) set provides a practical combination of robust internal turning holders for demanding bore machining. With the proven S-clamping system and a 93° approach angle, this tool system is excellently suited for precise internal turning and profiling on CNC and conventional lathes.
| Tap Typ | HSS-E-TiN |
| Hole | Trough Hole |
| Thread | Metric |
| Length | Jobber |
| Materials | Steel, Stainless Steel, Cast Iron and NF-Materials |
| Flank Angle | 60° |
| Packaging unit | 1 Pc. |
This complete set of HSS-E taps and perfectly matched core hole drills provides a practical solution for producing metric internal threads. Specifically designed for through holes, the TiN-coated tools support efficient and consistent machining processes in professional metalworking.
| Set consists of: | |
| Set 4 mm R | 1x SL1604, 1X E04G-SCLCR-03 und 5x CCGT 030102L RT200 |
| Set 4 mm L | 1x SL1604, 1X E04G-SCLCL-03 und 5x CCGT 030102R RT200 |
| Set 5 mm R | 1x SL1605, 1X E05H-SCLCR-03 und 5x CCGT 030102L RT200 |
| Set 5 mm L | 1x SL1605, 1X E05H-SCLCL-03 und 5x CCGT 030102R RT200 |
| Set 6 mm R | 1x SL1606, 1X E06J-SCLCR-03 und 5x CCGT 030102L RT200 |
| Set 6 mm L | 1x SL1606, 1X E06J-SCLCL-03 und 5x CCGT 030102R RT200 |
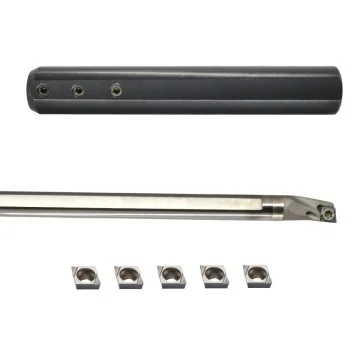
The solid carbide small boring bars sets provide professional users with a comprehensive tooling package for demanding internal turning in miniature components. Each set includes a highly precise solid carbide boring bar, the appropriate tool holder, and five high-performance indexable inserts of the RT200 grade. This well-thought-out combination supports efficient workflows during fine machining and opens up flexible applications for minimum bore diameters starting at 5 mm.
Packaging Unit = 1 Pc.

| Mill Typ | Solid Carbide End mill Set |
| Spiral Angle | 35°/38° |
| Material | Steel, Stainless Steel, Cast Iron |
| Processing | Roughing and Finish |
| Length | Standard Lenght |
| Shaft | Weldon Shaft |
| Teeth | 4 |
| Coating | RT405: PVD-TiAlN-coated high-performance grade for solid carbide milling cutters |
| Packaging unit | 1 Pc |
| d(h6) | d1 | H | M | L | Z | |
| 6 | 6 | 5,7 | 13 | 21 | 57 | 4 |
| 8 | 8 | 7,7 | 19 | 27 | 63 | 4 |
| 10 | 10 | 9,5 | 22 | 32 | 72 | 4 |
| 12 | 12 | 11,5 | 26 | 38 | 83 | 4 |
The Solid Carbide HPC Mill Set 6 - 12 mm provides four powerful end mills for efficient roughing and finishing operations. Featuring an unevenly divided 35°/38° spiral and the highly wear-resistant RT405 PVD-TiAlN coating, this set supports reliable and low-vibration milling in steel, stainless steel, and cast iron.


| d(h6) | d1 | H | M | L | Z | |
| 6 | 6 | 5,7 | 13 | 21 | 57 | 4 |
| 8 | 8 | 7,7 | 19 | 27 | 63 | 4 |
| 10 | 10 | 9,5 | 22 | 32 | 72 | 4 |
| 12 | 12 | 11,5 | 26 | 38 | 83 | 4 |
| 16 | 16 | 15,5 | 32 | 44 | 92 | 4 |
This 5-piece solid carbide milling set provides a practical selection of tools with diameters ranging from 6 to 16 mm. Designed for demanding roughing and finishing operations, these HPC mills are tailored to support efficient workflows and high process stability in professional machining.
| d | H | L | f | Dmin | |
| A10H SDUCR/L-07 with cooling holes | 10 | 09 | 100 | 08 | ≥13 |
| A12H SDUCR/L-07 with cooling holes | 12 | 11 | 100 | 10 | ≥16 |
| A16M SDUCR/L-11 with cooling holes | 16 | 15 | 150 | 13 | ≥21 |
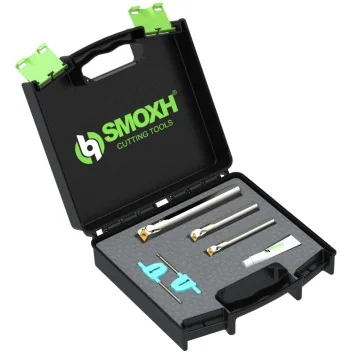
The A-SDUCR/L (93°) Set Inside turning holders with cooling holes by SMOXH is designed for professional use and provides a reliable solution for internal contour machining. The integrated coolant supply supports optimal chip evacuation and temperature control. Each set consists of three boring bars (A10H, A12H, A16M) in either right-hand (Art. Nr. SM59856) or left-hand (Art. Nr. SM59863) execution. Packaging Unit = 1 Pc.
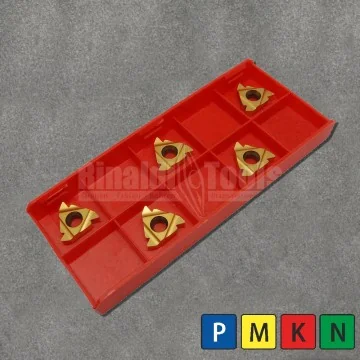
The Set 4 - 16ER-V-... RT330 (Universal) includes five high-quality indexable inserts for producing metric ISO threads. Covering pitches of 1.0, 1.5, 2.0, 2.5, and 3.0 mm, this compilation meets the most common requirements in thread manufacturing. The ER design is specifically tailored for cutting external threads. Thanks to the PVD-coated universal RT330 grade (P15-P25, M10-M25), the set is highly suitable for machining steel and stainless steel. The full-profile geometry supports the formation of precise thread profiles and enables efficient workflows in professional turning operations.

This three-piece end mill set is a professional solution for versatile machining tasks. Featuring a practical range of diameters from 12 mm to 20 mm and a standardized Weldon shank, this tool holder system creates optimal conditions for efficient workflows in industrial milling.