
 Deutsch
 English
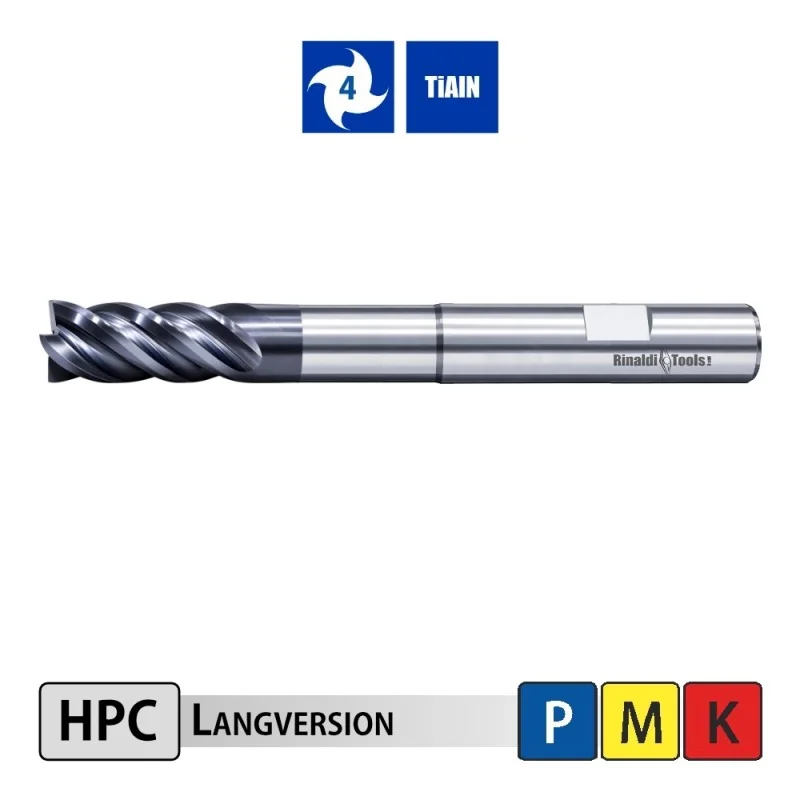
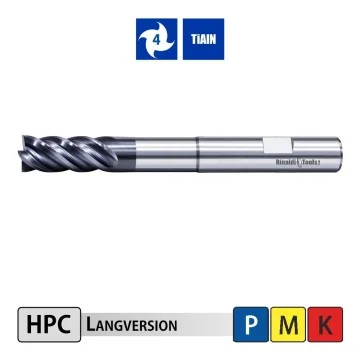
| Mill Type | Solid Carbide End mill |
| Helix Angle | 35°/38° |
| Workpiece Material | Steel, Stainless Steel, Cast Iron |
| Processing | Roughing and Finish |
| Length | Long version |
| Shaft | Weldon Shaft |
| Flutes | 4 |
| Grade | RT405: PVD-TiAlN-coated high-performance grade for solid carbide milling cutters |
| Packaging unit | 1 Pc |
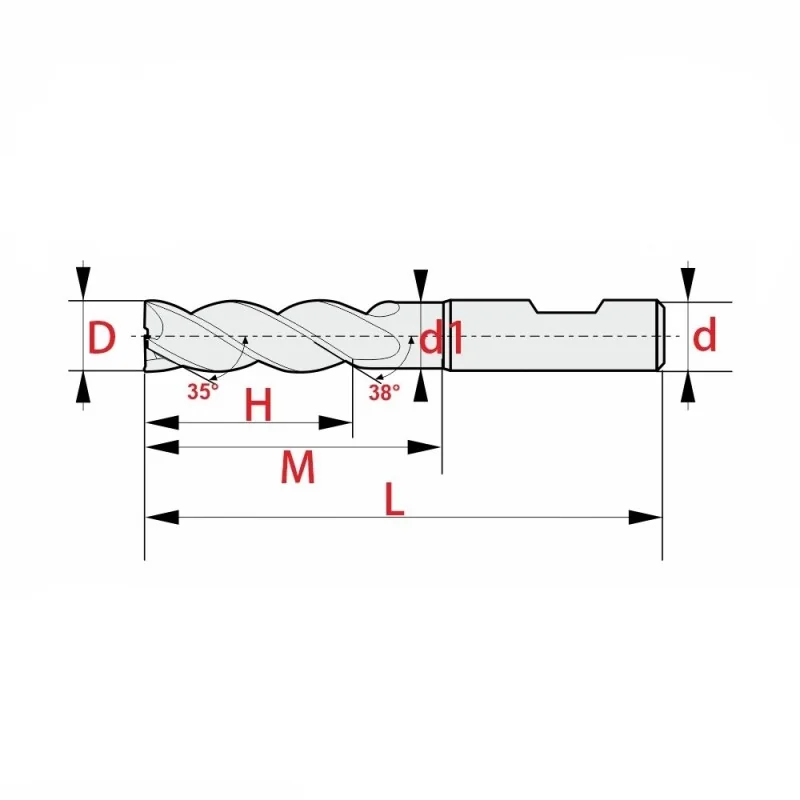
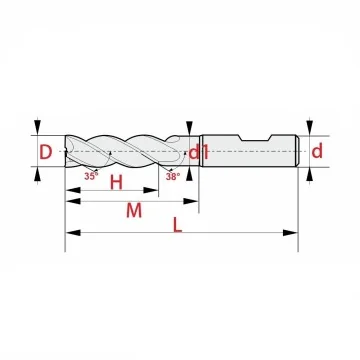
| D | d(h6) | d1 | H | M | L | Z | |
| HPCL-Z4-D3.0-W RT405 |
3 | 6 | 2,7 | 6,5 | 15 | 58 | 4 |
| HPCL-Z4-D4.0-W RT405 |
4 | 6 | 3,7 | 8,5 | 20 | 62 | 4 |
| HPCL-Z4-D5.0-W RT405 |
5 | 6 | 4,7 | 10,5 |
25 | 70 | 4 |
| HPCL-Z4-D6.0-W RT405 |
6 | 6 | 5,7 | 13 |
30 | 70 | 4 |
| HPCL-Z4-D8.0-W RT405 |
8 | 8 | 7,7 | 17 |
40 | 80 | 4 |
| HPCL-Z4-D10.0-W RT405 |
10 | 10 | 9,5 |
21 |
50 | 94 | 4 |
| HPCL-Z4-D12.0-W RT405 |
12 | 12 | 11,5 | 25 | 60 | 109 | 4 |
| HPCL-Z4-D16.0-W RT405 |
16 | 16 | 15,5 | 33 | 80 | 132 | 4 |
| HPCL-Z4-D20.0-W RT405 |
20 | 20 | 19,5 | 55 | 98 | 150 | 4 |
The solid carbide HPC mill with neck relief in the long version is a well-conceived tooling solution for professional applications. Designed for demanding roughing and finishing operations in steel, stainless steel, and cast iron, it delivers precise results. The long design combined with the neck relief opens up flexible application possibilities, especially for deep-seated and hard-to-reach workpiece contours. The four center-cutting flutes also ensure efficient workflows for various milling operations like ramping and plunging.


This four-flute solid carbide HPC end mill in the long version is precisely designed for machining demanding cavities and deep-lying form elements. By combining a Weldon shank with a specific neck relief, clearance contours are easily navigated. The cutting tool features an unequally pitched helix, which promotes smooth operation. Thanks to the RT405 PVD-TiAlN coating, users benefit from reliable wear protection, making this end mill a solid choice for modern roughing and finishing applications.
| Art. Nr. | D | d(h6) | d1 | H | M | L | Z | |
| HPCL-Z4-D3.0-W RT405 |
2551615 | 3 | 6 | 2,7 | 6,5 | 15 | 58 | 4 |
| HPCL-Z4-D4.0-W RT405 |
2551616 | 4 | 6 | 3,7 | 8,5 | 20 | 62 | 4 |
| HPCL-Z4-D5.0-W RT405 |
2551617 | 5 | 6 | 4,7 | 10,5 |
25 | 70 | 4 |
| HPCL-Z4-D6.0-W RT405 |
2551618 | 6 | 6 | 5,7 | 13 |
30 | 70 | 4 |
| HPCL-Z4-D8.0-W RT405 |
2551619 | 8 | 8 | 7,7 | 17 |
40 | 80 | 4 |
| HPCL-Z4-D10.0-W RT405 |
2551620 | 10 | 10 | 9,5 |
21 |
50 | 94 | 4 |
| HPCL-Z4-D12.0-W RT405 |
2551621 | 12 | 12 | 11,5 | 25 | 60 | 109 | 4 |
| HPCL-Z4-D16.0-W RT405 |
2551622 | 16 | 16 | 15,5 | 33 | 80 | 132 | 4 |
| HPCL-Z4-D20.0-W RT405 |
2551623 | 20 | 20 | 19,5 | 55 | 98 | 150 | 4 |
| Ae | Cutting speed | Feed fz [mm/z] | ||||||
| Vc[m/min] | Ø 3-5 | Ø 6-8 | Ø 10 | Ø 12-16 | Ø 20 | |||
| Structural Steel | <450 | 1/1 | 170-200 | 0,05-0,06 | 0,06-0,07 | 0,07 | 0,07-0,08 | 0,08 |
| 1/2 | 190-230 | 0,07-0,08 | 0,08-0,09 | 0,09 | 0,09-0,1 | 0,1 | ||
| 1/10 | 200-280 | 0,12-0,14 | 0,14-0,18 | 0,22 | 0,23-0,27 | 0,32-0,36 | ||
Tempered Steel |
450-700 |
1/1 | 130-190 | 0,05-0,06 | 0,06-0,07 | 0,07 | 0,07-0,08 | 0,08 |
| 1/2 | 160-210 | 0,07-0,08 | 0,08-0,09 | 0,09 | 0,09-0,1 | 0,1 | ||
| 1/10 | 180-220 | 0,12-0,14 | 0,14-0,18 | 0,22 | 0,23-0,27 | 0,32-0,36 | ||
| Tooling Steel | >700 | 1/1 | 120-180 | 0,05-0,06 | 0,06-0,07 | 0,07 | 0,07-0,08 | 0,08 |
| 1/2 | 150-200 | 0,07-0,08 | 0,08-0,09 | 0,09 | 0,09-0,1 | 0,1 | ||
| 1/10 | 170-220 | 0,12-0,14 | 0,14-0,18 | 0,22 | 0,23-0,27 | 0,32-0,36 | ||
| Stainless Steel | <1100 | 1/1 | 60-90 | 0,05 | 0,05 | 0,05 | 0,05-0,06 | 0,06 |
| 1/2 | 80-100 | 0,06 | 0,06-0,07 | 0,07 | 0,07-0,08 | 0,08 | ||
| 1/10 | 100-130 | 0,1 | 0,1-0,12 | 0,12 | 0,14-0,16 | 0,18 | ||
| Cast Iron | 1/1 | 150-200 | 0,06 | 0,06-0,07 | 0,07 | 0,07-0,08 | 0,08 | |
| 1/2 | 160-240 | 0,08 | 0,09 | 0,09 | 0,09-0,10 | 0,10 | ||
| 1/10 | 220-280 | 0,14-0,16 | 0,15-0,18 | 0,22 | 0,25-0,27 | 0,36 | ||
| Hardened Steel up to 55 HRC | 1/1 | 100 | 0,045-0,053 | 0,045-0,053 | 0,053 | 0,053-0,06 | 0,06 | |
| 1/2 | 120 | 0,06-0,07 | 0,06-0,07 | 0,07 | 0,07-0,08 | 0,08 | ||
| 1/10 | 140 | 0,1-0,12 | 0,1-0,12 | 0,12-0,14 | 0,16 | 0,18 | ||
This end mill is specifically designed for machining structural steel, tempered steel, tool steel, stainless steel, and cast iron. The extended design and integrated neck relief show their strengths especially when milling deep slots, pockets, and complex component contours. In addition to classic operations like shoulder and face milling, the tool is also suited for ramping and plunge milling due to its center-cutting capabilities.
A key feature of this tool is its vibration-reducing design. The unequal helix angle of 35°/38° counteracts harmonic oscillations and creates favorable conditions for excellent surface finishes on the workpiece. The combination of a tough solid carbide substrate and a robust TiAlN coating supports efficient machining processes with consistent results.
Data sheet
| Mill Type | Solid Carbide End mill |
| Helix Angle | 35°/38° |
| Workpiece Material | Steel, Stainless Steel, Cast Iron |
| Processing | Roughing and Finish |
| Length | Long version |
| Shaft | Weldon Shaft |
| Flutes | 4 |
| Grade | RT405: PVD-TiAlN-coated high-performance grade for solid carbide milling cutters |
| Packaging unit | 1 Pc |
| D | d(h6) | d1 | H | M | L | Z | |
| HPCL-Z4-D3.0-W RT405 |
3 | 6 | 2,7 | 6,5 | 15 | 58 | 4 |
| HPCL-Z4-D4.0-W RT405 |
4 | 6 | 3,7 | 8,5 | 20 | 62 | 4 |
| HPCL-Z4-D5.0-W RT405 |
5 | 6 | 4,7 | 10,5 |
25 | 70 | 4 |
| HPCL-Z4-D6.0-W RT405 |
6 | 6 | 5,7 | 13 |
30 | 70 | 4 |
| HPCL-Z4-D8.0-W RT405 |
8 | 8 | 7,7 | 17 |
40 | 80 | 4 |
| HPCL-Z4-D10.0-W RT405 |
10 | 10 | 9,5 |
21 |
50 | 94 | 4 |
| HPCL-Z4-D12.0-W RT405 |
12 | 12 | 11,5 | 25 | 60 | 109 | 4 |
| HPCL-Z4-D16.0-W RT405 |
16 | 16 | 15,5 | 33 | 80 | 132 | 4 |
| HPCL-Z4-D20.0-W RT405 |
20 | 20 | 19,5 | 55 | 98 | 150 | 4 |
The solid carbide HPC mill with neck relief in the long version is a well-conceived tooling solution for professional applications. Designed for demanding roughing and finishing operations in steel, stainless steel, and cast iron, it delivers precise results. The long design combined with the neck relief opens up flexible application possibilities, especially for deep-seated and hard-to-reach workpiece contours. The four center-cutting flutes also ensure efficient workflows for various milling operations like ramping and plunging.

| Mill Type | Solid Carbide Ball Nose Cutter |
| Helix Angle | 30° |
| Workpiece Material | Steel, Stainless Steel, Cast Iron |
| Processing | Medium and Finish |
| Lenght | Standard Lenght |
| Shank | Cylindrical Shank |
| Flutes | 4 |
| Grade | RT405: PVD-TIALN-coated high-performance grade for solid carbide milling cutters |
| Packaging unit | 1 Pc |
| D | r | d(h6) | H | L | Z | |
| KF-Z4-D3.0 RT405 | 3 | 1,5 | 6 | 6 | 50 | 4 |
| KF-Z4-D4.0 RT405 | 4 | 2 | 6 | 8 | 50 | 4 |
| KF-Z4-D5.0 RT405 | 6 | 2,5 | 6 | 10 | 50 | 4 |
| KF-Z4-D6.0 RT405 | 6 | 3 | 6 | 12 | 50 | 4 |
| KF-Z4-D8.0 RT405 | 8 | 4 | 8 | 16 | 60 | 4 |
| KF-Z4-D10.0 RT405 | 10 | 5 | 10 | 20 | 75 | 4 |
| KF-Z4-D12.0 RT405 | 12 | 6 | 12 | 24 | 75 | 4 |
| KF-Z4-D14.0 RT405 | 14 | 7 | 14 | 28 | 75 | 4 |
| KF-Z4-D16.0 RT405 | 16 | 8 | 16 | 32 | 100 | 4 |
| KF-Z4-D18.0 RT405 | 18 | 9 | 18 | 36 | 100 | 4 |
| KF-Z4-D20.0 RT405 | 20 | 10 | 20 | 40 | 100 | 4 |
The 4-flute solid carbide ball nose cutter is a practical choice for precise profile milling, copy milling, and medium finishing operations. With its 30° helix angle and centre-cutting face geometry, it opens up flexible application options in steel, stainless steel, and cast iron. The high-quality RT405 grade with PVD-TiAlN coating provides a solid foundation for consistent performance in professional tool and mould making. 
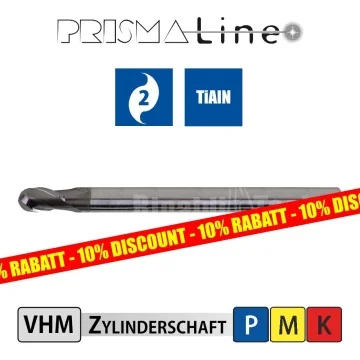
| Mill Type | Solid Carbide Ball Nose Cutter |
| Helix Angle | 30° |
| Workpiece Material | Steel, Stainless Steel, Cast Iron |
| Processing | Finish |
| Lenght | Long Version |
| Shank | Cylindrical Shank |
| Flutes | 2 |
| Grade | RT303: PVD-coated fine-grain carbide for general Application in milling (VHM) |
| Packaging unit | 1 Pc |
- 2-Flute Solid Carbide Ball Nose Cutter
- Centre Cutting
- PVD-Coated
| D | r | d(h6) | H | L | Z | Version | |
| KFL-P-Z2-D2.0 RT303 | 2 | 1 | 6 | 4 | 75 | 2 | A |
| KFL-P-Z2-D2.5 RT303 | 2,5 | 1,25 | 6 | 5 | 75 | 2 | A |
| KFL-P-Z2-D3.0 RT303 |
3 | 1,5 | 6 | 6 | 75 | 2 | A |
| KFL-P-Z2-D3.5 RT303 | 3,5 | 1,75 | 6 | 8 | 75 | 2 | A |
| KFL-P-Z2-D4.0 RT303 |
4 | 2 | 6 | 8 | 75 | 2 | A |
| KFL-P-Z2-D5.0 RT303 |
5 | 2,5 | 6 | 10 | 75 | 2 | A |
| KFL-P-Z2-D6.0 RT303 |
6 | 3 | 6 | 12 | 75 | 2 | B |
| KFL-P-Z2-D8.0 RT303 |
8 | 4 | 8 | 16 | 75 | 2 | B |
| KFL-P-Z2-D10.0 RT303 |
10 | 5 | 10 | 20 | 100 | 2 | B |
| KFL-P-Z2-D12.0 RT303 |
12 | 6 | 12 | 24 | 100 | 2 | B |
| KFL-P-Z2-D16.0 RT303 | 16 | 8 | 16 | 32 | 150 | 2 | B |
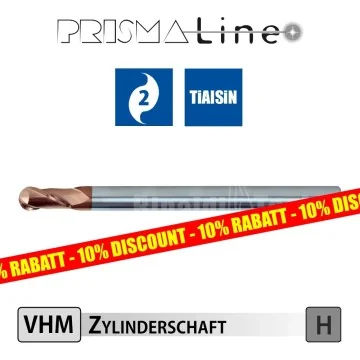
| Mill Type | Solid Carbide Ball Nose Hard Cutter |
| Helix Angle | 35° |
| Workpiece Material | Hard Materials up to 68 HRC |
| Lenght | Long Version |
| Shank | Cylindrical Shank |
| Flutes | 2 |
| Grade | RT555: PVD-coated carbide substrate for the Hard machining of steel (up to HRC 55-68). Highest wear resistance and toughness |
| Packaging unit | 1 Pc. |
- 2-Flute Solid Carbide Ball Nose Cutter
- Centre Cutting
- PVD-coated
| D | r | d(h6) | H | L | Z | Version | |
| HKFL-P-Z2-D2.0 RT555 | 2 | 1 | 6 | 4 | 75 | 2 | A |
| HKFL-P-Z2-D2.5 RT555 |
2,5 | 1,25 | 6 | 6 | 75 | 2 | A |
| HKFL-P-Z2-D3.0 RT555 |
3 | 1,5 | 6 | 6 | 75 | 2 | A |
| HKFL-P-Z2-D3.5 RT555 |
3,5 | 1,75 | 6 | 8 | 75 | 2 | A |
| HKFL-P-Z2-D4.0 RT555 |
4 | 2 | 6 | 8 | 75 | 2 | A |
| HKFL-P-Z2-D5.0 RT555 |
5 | 2,5 | 6 | 10 | 75 | 2 | A |
| HKFL-P-Z2-D6.0 RT555 |
6 | 3 | 6 | 12 | 75 | 2 | B |
| HKFL-P-Z2-D8.0 RT555 |
8 | 4 | 8 | 16 | 75 | 2 | B |
| HKFL-P-Z2-D10.0 RT555 |
10 | 5 | 10 | 20 | 100 | 2 | B |
| HKFL-P-Z2-D12.0 RT555 |
12 | 6 | 12 | 24 | 100 | 2 | B |
| HKFL-P-Z2-D16.0 RT555 |
16 | 8 | 16 | 32 | 150 | 2 | B |
| HKFL-P-Z2-D20.0 RT555 |
20 | 10 | 20 | 40 | 150 | 2 | B |
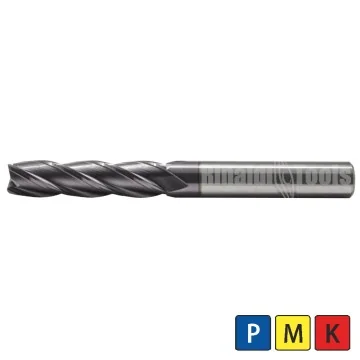
| Mill Type | Solid Carbide End mill |
| Helix Angle | 30° |
| Workpiece Materials | Steel, Stainless Steel, Cast Iron |
| Processing | Finish |
| Lenght | Extra long cutting Edge |
| Shaft | Cylindrical Shaft |
| Flutes | 4 |
| Grade | RT405: PVD-TIALN-coated high-performance grade for solid carbide milling cutters |
| Packaging unit | 1 Pc |
- 4-Flute Solid Carbide Cutter
- Centre Cutting
- TIALN-Coated
| D | d | H | L | Z | Version | |
| SFX-Z4-D3.0 RT405 | 3 | 6 | 20 | 75 | 4 | A |
| SFX-Z4-D4.0 RT405 | 4 | 6 | 25 | 75 | 4 | A |
| SFX-Z4-D5.0 RT405 | 5 | 6 | 30 | 75 | 4 | A |
| SFX-Z4-D6.0 RT405 | 6 | 6 | 30 | 75 | 4 | B |
| SFX-Z4-D8.0 RT405 | 8 | 8 | 40 | 100 | 4 | B |
| SFX-Z4-D10.0 RT405 | 10 | 10 | 50 | 110 | 4 | B |
| SFX-Z4-D12.0 RT405 | 12 | 12 | 50 | 110 | 4 | B |
| SFX-Z4-D16.0 RT405 | 16 | 16 | 70 | 150 | 4 | B |
| SFX-Z4-D20.0 RT405 | 20 | 20 | 75 | 150 | 4 | B |

| Mill Type | Solid Carbide Undersize Milling Cutter |
| Helix Angle | 30° |
| Workpiece Material | Steel, Stainless Steel, Cast Iron |
| Processing | Medium |
| Lenght | Standard Lenght |
| Shank | Weldon-Shank |
| Flutes | 2 |
| Grade | RT405: PVD-coated fine-grain carbide for general Application in milling (VHM) |
| Packaging unit | 1 Pc |
| D | d(h6) | H | L | Z | |
| 2,8 | 2,8 | 6 | 7 | 57 | 2 |
| 3,8 | 3,8 | 6 | 8 | 57 | 2 |
| 4,8 | 4,8 | 6 | 8 | 57 | 2 |
| 5,75 | 5,75 | 6 | 10 | 57 | 2 |
| 7,75 | 7,75 | 8 | 16 | 63 | 2 |
| 8,7 | 8,7 | 10 | 16 | 72 | 2 |
| 11,7 | 11,7 | 12 | 22 | 83 | 2 |
| 13,7 | 13,7 | 14 | 22 | 83 | 2 |
| 15,7 | 15,7 | 16 | 26 | 92 | 2 |
This 2-flute solid carbide undersize milling cutter is specially designed for machining precise slots and keyways. With its centre-cutting geometry and reliable Weldon shank, the tool ensures excellent process stability in steel, stainless steel, and cast iron. It is perfectly suited for various medium milling strategies and preparing accurate fits.
| d(h6) | d1 | H | M | L | Z | |
| 6 | 6 | 5,7 | 13 | 21 | 57 | 4 |
| 8 | 8 | 7,7 | 19 | 27 | 63 | 4 |
| 10 | 10 | 9,5 | 22 | 32 | 72 | 4 |
| 12 | 12 | 11,5 | 26 | 38 | 83 | 4 |
| 16 | 16 | 15,5 | 32 | 44 | 92 | 4 |
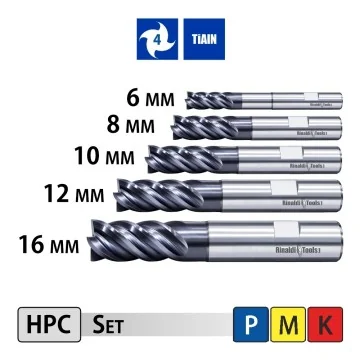
This 5-piece solid carbide milling set provides a practical selection of tools with diameters ranging from 6 to 16 mm. Designed for demanding roughing and finishing operations, these HPC mills are tailored to support efficient workflows and high process stability in professional machining.
| Mill Type | Solid Carbide End Mill |
| Helix Angle | 55° |
| Workpiece Material | NF-Materials |
| Lenght | Long Version |
| Shank | Cylindrical Shank |
| Flutes | 2 |
| Grade | RT30K: Uncoated K30 carbide substrate for machining non-ferrous metals |
| Packaging unit | 1 Pc |
| D | d(h6) | H | L | Z | Version | |
| AFL-Z2-D3.0 RT30K | 3 | 6 | 12 | 60 | 2 | A |
| AFL-Z2-D4.0 RT30K | 4 | 6 | 16 | 60 | 2 | A |
| AFL-Z2-D5.0 RT30K | 5 | 6 | 20 | 60 | 2 | A |
| AFL-Z2-D6.0 RT30K | 6 | 6 | 25 | 75 | 2 | B |
| AFL-Z2-D8.0 RT30K | 8 | 8 | 32 | 75 | 2 | B |
| AFL-Z2-D10.0 RT30K | 10 | 10 | 45 | 100 | 2 | B |
| AFL-Z2-D12.0 RT30K | 12 | 12 | 45 | 100 | 2 | B |
| AFL-Z2-D16.0 RT30K | 16 | 16 | 65 | 150 | 2 | B |
| AFL-Z2-D20.0 RT30K | 20 | 20 | 75 | 150 | 2 | B |
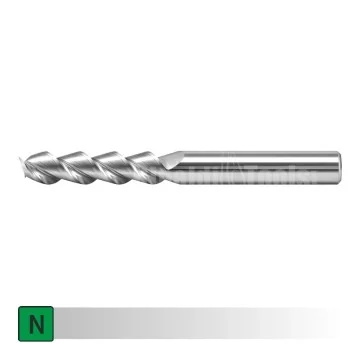
The 2-flute solid carbide end mill in the long version is specifically designed for the demanding machining of aluminum and other non-ferrous materials. Thanks to its extended design, it easily reaches deep machining areas, while the 55° helix angle ensures excellent chip evacuation. The uncoated K30 carbide substrate RT30K reliably prevents built-up edges and supports highly efficient workflows.
| Mill Typ | Solid Carbide roughing mill for Aluminum |
| Spiral Angle | 30° |
| Material | NF-Materials |
| Processing | Roughing |
| Shaft | Cylinder Shaft |
| Flutes | 3 |
| Grade | RT30K: Uncoated K30 carbide substrate for processing non-ferrous metals |
| Packaging unit | 1 Pc |
| D | d | H | L | Corner bevel | |
| AFR-Z3-D6.0 RT30K | 6,0 | 6 | 16 | 57 | 0,60 |
| AFR-Z3-D7.0 RT30K | 7,0 | 8 | 16 | 63 | 0,60 |
| AFR-Z3-D8.0 RT30K | 8,0 | 8 | 16 | 63 | 0,60 |
| AFR-Z3-D9.0 RT30K |
9,0 | 10 | 19 | 72 | 0,60 |
| AFR-Z3-D10.0 RT30K | 10,0 | 10 | 22 | 72 | 0,60 |
| AFR-Z3-D12.0 RT30K |
12,0 | 12 | 26 | 83 | 0,60 |
| AFR-Z3-D14.0 RT30K | 14,0 | 14 | 26 | 83 | 0,91 |
| AFR-Z3-D16.0 RT30K | 16,0 | 16 | 32 | 92 | 0,91 |
| AFR-Z3-D18.0 RT30K | 18,0 | 18 | 32 | 92 | 0,91 |
| AFR-Z3-D20.0 RT30K | 20,0 | 20 | 38 | 104 | 0,91 |
| AFR-Z3-D25.0 RT30K | 25,0 | 25 | 45 | 121 | 0,91 |
The Solid Carbide Aluminum Roughing Mill with 3 flutes and a cylinder shaft is designed for high material removal in aluminum and non-ferrous metals. The uncoated RT30K substrate and 30° spiral angle support efficient workflows and rapid chip evacuation. Additionally, the centre cutting design opens up flexible application options.
| Mill Type | Solid Carbide Ball Nose Cutter |
| Helix Angle | 30° |
| Workpiece Material | Steel, Stainless Steel, Cast Iron |
| Processing | Finish |
| Lenght | Extra Long Shank |
| Shank | Cylindrical Shank |
| Flutes | 2 |
| Grade | RT303: PVD-coated fine-grain carbide for general Application in milling (VHM) |
| Packaging unit | 1 Pc |
- 2-Flute Solid Carbide Ball Nose Cutter
- Centre Cutting
- PVD-Coated
| D | r | d(h6) | H | L | Z | |
| KFEL-P-Z2-D6.0 RT303 | 6 | 3 | 6 | 12 | 100 | 2 |
| KFEL-P-Z2-D8.0 RT303 | 8 | 4 | 8 | 16 | 100 | 2 |
| KFEL-P-Z2-D10.0 RT303 | 10 | 5 | 10 | 20 | 150 | 2 |
| KFEL-P-Z2-D12.0 RT303 | 12 | 6 | 12 | 24 | 150 | 2 |
| Mill Type | Solid Carbide Hard Milling Cutter |
| Helix Angle | 45° |
| Workpiece Material | Hard Materials up to 68 HRC |
| Lenght | Standard Length |
| Shank | Cylindrical Shank |
| Flutes | 4 |
| Grade | RT555: PVD-coated carbide substrate for the Hard machining of steel (up to HRC 55-68). Highest wear resistance and toughness |
| Packaging unit | 1 Pc |
- 4-Flute Solid Carbide Hard Milling Cutter
- Centre Cutting
- PVD-Coated
| D | d(h6) | H | L | Z | Version | |
| HF-P-Z4-D1.0 RT555 | 1 | 6 | 3 | 50 | 4 | A |
| HF-P-Z4-D2.0 RT555 |
2 | 6 | 6 | 50 | 4 | A |
| HF-P-Z4-D3.0 RT555 |
3 | 6 | 8 | 50 | 4 | A |
| HF-P-Z4-D3.5 RT555 | 3,5 | 6 | 10 | 50 | 4 | A |
| HF-P-Z4-D4.0 RT555 |
4 | 6 | 11 | 50 | 4 | A |
| HF-P-Z4-D5.0 RT555 |
5 | 6 | 13 | 50 | 4 | A |
| HF-P-Z4-D6.0 RT555 |
6 | 6 | 16 | 50 | 4 | B |
| HF-P-Z4-D8.0 RT555 |
8 | 8 | 20 | 60 | 4 | B |
| HF-P-Z4-D10.0 RT555 |
10 | 10 | 25 | 75 | 4 | B |
| HF-P-Z4-D12.0 RT555 |
12 | 12 | 30 | 75 | 4 | B |
| HF-P-Z4-D14.0 RT555 |
14 | 14 | 32 | 75 | 4 | B |
| HF-P-Z4-D16.0 RT555 |
16 | 16 | 45 | 100 | 4 | B |
| HF-P-Z4-D20.0 RT555 |
20 | 20 | 45 | 100 | 4 | B |
| Mill Type | Solid Carbide Ball Nose Hard Milling Cutter |
| Helix Angle | 35° |
| Workpiece Material | Hard Materials up to 68 HRC |
| Lenght | Standard Length |
| Shank | Cylindrical Shank |
| Flutes | 2 |
| Grade | RT555: PVD-coated carbide substrate for the Hard machining of steel (up to HRC 55-68). Highest wear resistance and toughness |
| Packaging unit | 1 Pc. |
- 2-Flute Solid Carbide Ball Nose Hard Milling Cutter
- Centre Cutting
- PVD-Coated
| r | D | d(h6) | H | L | Z | Version | |
| HKF-P-Z2-D1.5 RT555 | 0,75 | 1,5 | 4 | 3 | 50 | 2 | A |
| HKF-P-Z2-D2.0 RT555 | 1 | 2 | 6 | 4 | 50 | 2 | A |
| HKF-P-Z2-D2.5 RT555 |
1,25 | 2,5 | 6 | 5 | 50 | 2 | A |
| HKF-P-Z2-D3.0 RT555 |
1,5 | 3 | 6 | 6 | 50 | 2 | A |
| HKF-P-Z2-D3.5 RT555 | 1,75 | 3,5 | 6 | 8 | 50 | 2 | A |
| HKF-P-Z2-D4.0 RT555 |
2 | 4,0 | 6 | 8 | 50 | 2 | A |
| HKF-P-Z2-D5.0 RT555 |
2,5 | 5,0 | 6 | 10 | 50 | 2 | A |
| HKF-P-Z2-D6.0 RT555 |
3 | 6 | 6 | 12 | 50 | 2 | B |
| HKF-P-Z2-D8.0 RT555 |
4 | 8 | 8 | 16 | 60 | 2 | B |
| HKF-P-Z2-D10.0 RT555 |
5 | 10 | 10 | 20 | 75 | 2 | B |
| HKF-P-Z2-D12.0 RT555 |
6 | 12 | 12 | 24 | 75 | 2 | B |
| HKF-P-Z2-D16.0 RT555 |
8 | 16 | 16 | 32 | 100 | 2 | B |
| HKF-P-Z2-D20.0 RT555 |
10 | 20 | 20 | 40 | 100 | 2 | B |
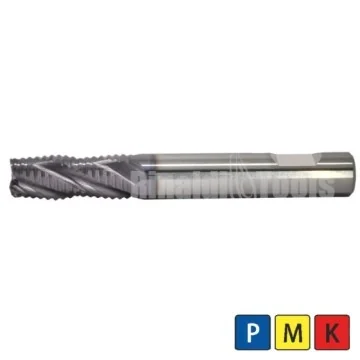
| Mill Type | Solid Carbide Roughing Mill |
| Helix Angle | 30° |
| Workpiece Material | Steel, Stainless Steel, Cast Iron |
| Processing | Roughing |
| Shank | Weldon Shank |
| Grade | RT405: PVD-TIALN-coated high-performance grade for solid carbide milling cutters |
| Packaging unit | 1 Pc |
| D | d(h5) | H | L | Z | |
| SFR-Z3-D6.0 RT405 | 6 | 6 | 16 | 57 | 3 |
| SFR-Z3-D8.0 RT405 | 8 | 8 | 16 | 63 | 3 |
| SFR-Z4-D10.0 RT405 | 10 | 10 | 22 | 72 | 4 |
| SFR-Z4-D12.0 RT405 | 12 | 12 | 26 | 83 | 4 |
| SFR-Z4-D14.0 RT405 | 14 | 14 | 26 | 83 | 4 |
| SFR-Z4-D16.0 RT405 | 16 | 16 | 32 | 92 | 4 |
| SFR-Z4-D18.0 RT405 | 18 | 18 | 32 | 92 | 4 |
| SFR-Z4-D20.0 RT405 | 20 | 20 | 38 | 104 | 4 |
| SFR-Z5-D25.0 RT405 | 25 | 25 | 45 | 121 | 5 |
This Solid Carbide Roughing Mill featuring a robust Weldon shank is a highly practical solution for professional operations requiring large chip volumes in steel, stainless steel, and cast iron. Coated with the high-performance RT405 PVD-TiAlN grade, this milling tool supports uninterrupted workflows and offers great wear resistance. Because of its centre cutting geometry, the tool enables direct axial plunging directly into the workpiece.
Provides flexible and reliable capabilities for these milling tasks:
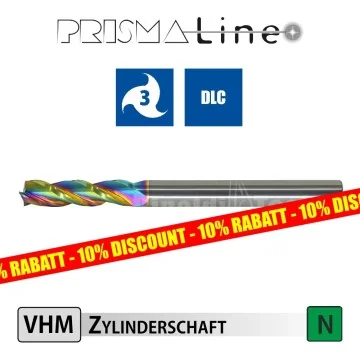
| Mill Type | Solid Carbide End Mill for Aluminum |
| Helix Angle | 35° |
| Workpiece Material | Non-Ferrous Metals |
| Lenght | Long Version |
| Shank | Cylindrical Shank |
| Flutes | 3 |
| Grade | RT107: The DLC coating (Diamond-Like Carbon) ensures higher wear resistance. |
| Packaging unit | 1 Pc |

- 3-Flute Solid Carbide End Mill
- Centre Cutting
| D | d | H | L | Z | Version | |
| AFL-P-Z3-D4.0 RT107 | 4 | 6 | 15 | 75 | 3 | A |
| AFL-P-Z3-D5.0 RT107 | 5 | 6 | 20 | 75 | 3 | A |
| AFL-P-Z3-D6.0 RT107 | 6 | 6 | 25 | 75 | 3 | B |
| AFL-P-Z3-D8.0 RT107 | 8 | 8 | 32 | 75 | 3 | B |
| AFL-P-Z3-D10.0 RT107 | 10 | 10 | 45 | 100 | 3 | B |
| AFL-P-Z3-D12.0 RT107 | 12 | 12 | 45 | 100 | 3 | B |
| AFL-P-Z3-D16.0 RT107 | 16 | 16 | 65 | 150 | 3 | B |
| AFL-P-Z3-D20.0 RT107 | 20 | 20 | 75 | 150 | 3 | B |
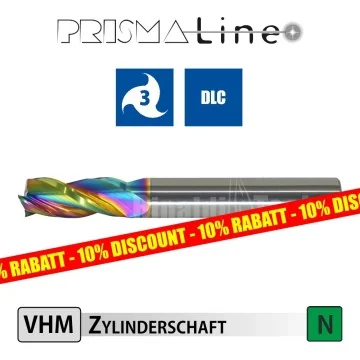
| Mill Type | Solid Carbide End Mill for Aluminum |
| Helix Angle | 35° |
| Workpiece Material | Non-Ferrous Metals |
| Lenght | Standard Lenght |
| Shank | Cylindrical Shank |
| Flutes | 3 |
| Grade | RT107: The DLC coating (Diamond-Like Carbon) ensures higher wear resistance. |
| Packaging unit | 1 Pc |
- 3-Flute Solid Carbide End Mill
- Centre Cutting
| D | d | H | L | Z | Version | |
| AF-P-Z3-D4.0 RT107 | 4 | 6 | 10 | 50 | 3 | A |
| AF-P-Z3-D5.0 RT107 | 5 | 6 | 13 | 50 | 3 | A |
| AF-P-Z3-D6.0 RT107 | 6 | 6 | 16 | 50 | 3 | B |
| AF-P-Z3-D8.0 RT107 | 8 | 8 | 20 | 60 | 3 | B |
| AF-P-Z3-D10.0 RT107 | 10 | 10 | 25 | 75 | 3 | B |
| AF-P-Z3-D12.0 RT107 | 12 | 12 | 30 | 75 | 3 | B |
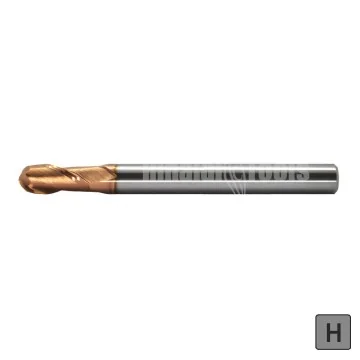
| Mill Type | Solid Carbide Ball Nose Hard Cutter |
| Helix Angle | 35° |
| Workpiece Material | Hard Materials up to 68 HRC |
| Lenght | Long Version |
| Shank | Cylindrical Shank |
| Flutes | 2 |
| Grade | RT555: PVD-coated carbide substrate for the Hard machining of steel (up to HRC 55-68). Highest wear resistance and toughness |
| Packaging unit | 1 Pc. |
- 2-Flute Solid Carbide Ball Nose Hard Cutter
- Centre Cutting
- PVD-Coated
| D | r | d(h6) | H | L | Z | |
| HKFL-Z2-D2.0 RT555 | 2 | 1 | 6 | 4 | 75 | 2 |
| HKFL-Z2-D2.5 RT555 | 2,5 | 1,25 | 6 | 6 | 75 |
2 |
| HKFL-Z2-D3.0 RT555 | 3 | 1,5 | 6 | 6 | 75 |
2 |
| HKFL-Z2-D3.5 RT555 | 3,5 | 1,75 | 6 | 8 | 75 |
2 |
| HKFL-Z2-D4.0 RT555 | 4 | 2 | 6 | 8 | 75 |
2 |
| HKFL-Z2-D5.0 RT555 | 5 | 2,5 | 6 | 10 | 75 | 2 |
| HKFL-Z2-D5.5 RT555 | 5,5 | 2,75 | 6 | 12 | 75 | 2 |
| HKFL-Z2-D6.0 RT555 | 6 | 3 | 6 | 12 | 75 | 2 |
| HKFL-Z2-D8.0 RT555 | 8 | 4 | 8 | 16 | 100 | 2 |
| HKFL-Z2-D10.0 RT555 | 10 | 5 | 10 | 20 | 100 | 2 |
| HKFL-Z2-D12.0 RT555 | 12 | 6 | 12 | 24 | 100 | 2 |
| HKFL-Z2-D14.0 RT555 | 14 | 7 | 14 | 28 | 100 | 2 |
| HKFL-Z2-D16.0 RT555 | 16 | 8 | 16 | 32 | 150 | 2 |
| HKFL-Z2-D20.0 RT555 | 20 | 10 | 20 | 40 | 150 | 2 |

| Mill Type | Solid Carbide Hard Torus Cutter |
| Helix Angle | 35° |
| Workpiece Material | Hard Materials up to 68 HRC |
| Lenght | Standard Lenght |
| Shank | Cylindrical Shank |
| Flutes | 4 |
| Grade | RT555: PVD-coated carbide substrate for the Hard machining of steel (up to HRC 55-68). Highest wear resistance and toughness |
| Packaging unit | 1 Pc. |
- 4-Flute Solid Carbide Torus Cutter
- Centre Cutting
- PVD-Coated
| D | r | d(h6) | H | L | Z | |
| HTFR-Z4-D3.0-R0.2 RT555 | 3 | 0,2 | 4 | 8 | 50 | 4 |
| HTFR-Z4-D4.0-R0.3 RT555 | 4 | 0,3 | 4 | 10 | 50 | 4 |
| HTFR-Z4-D4.0-R0.5 RT555 | 4 | 0,5 | 4 | 10 | 50 |
4 |
| HTFR-Z4-D5.0-R0.5 RT555 | 5 | 0,5 | 6 | 13 | 50 |
4 |
| HTFR-Z4-D5.0-R1.0 RT555 | 5 | 1 | 6 | 13 | 50 |
4 |
| HTFR-Z4-D6.0-R0.5 RT555 | 6 | 0,5 | 6 | 16 | 50 |
4 |
| HTFR-Z4-D6.0-R1,0 RT555 | 6 | 1 | 6 | 16 | 50 |
4 |
| HTFR-Z4-D8.0-R0,5 RT555 | 8 | 0,5 | 8 | 20 | 60 | 4 |
| HTFR-Z4-D8.0-R1,0 RT555 | 8 | 1 | 8 | 20 | 60 | 4 |
| HTFR-Z4-D10.0-R0.5 RT555 | 10 | 0,5 | 10 | 25 | 75 | 4 |
| HTFR-Z4-D10.0-R1.0 RT555 | 10 | 1 | 10 | 25 | 75 | 4 |
| HTFR-Z4-D10.0-R2.0 RT555 | 10 | 2 | 10 | 25 | 75 | 4 |
| HTFR-Z4-D10.0-R3.0 RT555 | 10 | 3 | 10 | 25 | 75 | 4 |
| HTFR-Z4-D12.0-R0,5 RT555 | 12 | 0,5 | 12 | 30 | 75 | 4 |
| HTFR-Z4-D12.0-R1.0 RT555 | 12 | 1 | 12 | 30 | 75 | 4 |
| HTFR-Z4-D12.0-R2.0 RT555 | 12 | 2 | 12 | 30 | 75 | 4 |
| HTFR-Z4-D12.0-R3.0 RT555 | 12 | 3 | 12 | 30 | 75 | 4 |