
 Deutsch
 English


| Tools | Inserts for interchangeable tip drills |
| Point Angle | 140° |
| Scope of Application | Steel and Cast Iron |
| Coating | RT19: CVD Coated P25/K20 Carbide Grade for universal drilling of steel and cast materials. |
| Packaging unit | 1 Pc |
| Item Nr. | Diameter | Holder | |
| WS-D22.00 RT19 | 3602200 | 22,00 |
WST-D22.0-3xD-H WST-D22.0-5xD-H WST-D22.0-8xD-H |
| WS-D22.10 RT19 | 3602210 | 22,10 | |
| WS-D22.20 RT19 | 3602220 | 22,20 | |
| WS-D22.23 RT19 | 3602223 | 22,23 | |
| WS-D22.30 RT19 | 3602230 | 22,30 | |
| WS-D22.40 RT19 | 3602240 | 22,40 | |
| WS-D22.50 RT19 | 3602250 | 22,50 | |
| WS-D22.60 RT19 | 3602260 | 22,60 | |
| WS-D22.62 RT19 | 3602262 | 22,62 | |
| WS-D22.70 RT19 | 3602270 | 22,70 | |
| WS-D22.80 RT19 | 3602280 | 22,80 | |
| WS-D22.90 RT19 | 3602290 | 22,90 |
The WS RT19 interchangeable drill tips in the diameter range of 22.00 to 22.90 mm are designed for professional drilling applications. They provide a solid foundation for machining steel and cast iron, helping to reduce setup times through an efficient interchangeable tip system.
Please pay attention to the holder/drill bit combinations!
These drill bits only fit the WST D22.0-..xD-H holder (22.00 to 22.90 mm).
The WS RT19 solid carbide interchangeable drill tips (diameter 22.00 to 22.90 mm) are designed to efficiently handle demanding drilling operations in industrial applications. Thanks to the practical interchangeable head system, they support quick tool changes directly on the machine, thereby reducing valuable setup time. The drill tips are precisely matched to the corresponding tool holders and offer excellent repeatability.
Please pay attention to the holder/drill bit combinations!
These drill bits only fit the WST D22.0-..xD-H holder (22.00 to 22.90 mm).
| Tools | Inserts for interchangeable tip drills |
| Point Angle | 140° |
| Scope of Application | Steel and Cast Iron |
| Coating | RT19: CVD Coated P25/K20 Carbide Grade for universal drilling of steel and cast materials. |
| Packaging unit | 1 Pc |
| Item Nr. | Diameter | Holder | |
| WS-D22.00 RT19 | 3602200 | 22,00 |
WST-D22.0-3xD-H WST-D22.0-5xD-H WST-D22.0-8xD-H |
| WS-D22.10 RT19 | 3602210 | 22,10 | |
| WS-D22.20 RT19 | 3602220 | 22,20 | |
| WS-D22.23 RT19 | 3602223 | 22,23 | |
| WS-D22.30 RT19 | 3602230 | 22,30 | |
| WS-D22.40 RT19 | 3602240 | 22,40 | |
| WS-D22.50 RT19 | 3602250 | 22,50 | |
| WS-D22.60 RT19 | 3602260 | 22,60 | |
| WS-D22.62 RT19 | 3602262 | 22,62 | |
| WS-D22.70 RT19 | 3602270 | 22,70 | |
| WS-D22.80 RT19 | 3602280 | 22,80 | |
| WS-D22.90 RT19 | 3602290 | 22,90 |
| ISO | VDI 3323 |
Material | Vc (m/min) | Feed (mm/rev) | |||||
| Ø10,00-11,99 | Ø12,09-14,99 | Ø15,00-17,99 | Ø18,00-21,99 | Ø22,00-26,99 | Ø27,00-33,99 | ||||
| P | 1 | Non-alloy steel | 100-126 | 0,14-0,24 | 0,18-0,31 | 0,23-0,39 | 0,30-0,44 | 0,37-0,57 | 0,41-0,61 |
| 2 | 84-110 | 0,12-0,21 | 0,15-0,26 | 0,23-0,39 | 0,30-0,44 | 0,37-0,57 | 0,41-0,61 | ||
| 3 | 63-84 | 0,11-0,81 | 0,13-0,22 | 0,19-0,31 | 0,24-0,35 | 0,33-0,51 | 0,36-0,54 | ||
| 4 | 58-74 | 0,09-0,14 | 0,11-0,18 | 0,17-0,28 | 0,23-0,33 | 0,28-0,42 | 0,32-0,47 | ||
| 5 | 58-74 | 0,09-0,14 | 0,11-0,18 | 0,17-0,28 | 0,23-0,33 | 0,28-0,42 | 0,32-0,47 | ||
| 6 | Low alloy steel | 74-95 | 0,11-0,18 | 0,13-0,22 | 0,19-0,31 | 0,24-0,35 | 0,33-0,51 | 0,37-0,55 | |
| 7 | 63-84 | 0,11-0,18 | 0,13-0,22 | 0,17-0,28 | 0,24-0,35 | 0,33-0,51 | 0,37-0,55 | ||
| 8 | 58-74 | 0,09-0,14 | 0,11-0,18 | 0,14-0,23 | 0,23-0,33 | 0,28-0,42 | 0,32-0,47 | ||
| 9 | 47-63 | 0,07-0,11 | 0,09-0,13 | 0,14-0,23 | 0,23-0,33 | 0,28-0,42 | 0,32-0,47 | ||
| 10 | High alloyed steel & tool steel |
53-68 | 0,09-0,14 | 0,11-0,18 | 0,14-0,23 | 0,20-0,29 | 0,22-0,34 | 0,26-0,39 | |
| 11 | 42-58 | 0,09-0,14 | 0,11-0,18 | 0,12-0,20 | 0,23-0,33 | 0,22-0,34 | 0,26-0,39 | ||
| K | 15 | Grey Cast Iron | 105-131 | 0,13-0,23 | 0,17-0,29 | 0,22-0,41 | 0,30-0,46 | 0,40-0,56 | 0,44-0,61 |
| 16 | 79-100 | 0,10-0,18 | 0,12-0,22 | 0,18-0,32 | 0,22-0,33 | 0,28-0,39 | 0,32-0,44 | ||
| 17 | Nodular Cast Iron | 100-126 | 0,11-0,20 | 0,14-0,24 | 0,19-0,34 | 0,23-0,35 | 0,31-0,44 | 0,35-0,48 | |
| 18 | 79-100 | 0,10-0,18 | 0,12-0,22 | 0,15-0,29 | 0,21-0,32 | 0,28-0,39 | 0,32-0,44 | ||
| 19 | Malleable Cast Iron | 105-131 | 0,11-0,20 | 0,14-0,24 | 0,19-0,34 | 0,23-0,35 | 0,31-0,44 | 0,35-0,48 | |
| 20 | 79-100 | 0,10-0,15 | 0,12-0,20 | 0,15-0,29 | 0,21-0,32 | 0,28-0,39 | 0,32-0,44 | ||
When using the 5xD or 8xD drill body, we recommend reducing the feed rate to 85% or 70%.
These solid carbide drill tips are specifically designed for the universal drilling of unalloyed, low-alloyed, and high-alloyed steel, as well as grey, nodular, and malleable cast iron. They prove particularly effective in medium to large production runs in mechanical engineering, where consistent performance and reliable hole quality are required.
The RT19 grade combines a tough P25/K20 carbide substrate with a highly wear-resistant CVD coating. This combination creates excellent conditions for long tool life and secure machining processes. The 140° point angle promotes precise centering and ensures an even distribution of cutting forces when processing robust materials.
| Tools | Inserts for interchangeable tip drills |
| Point Angle | 140° |
| Scope of Application | Steel and Cast Iron |
| Coating | RT19: CVD Coated P25/K20 Carbide Grade for universal drilling of steel and cast materials. |
| Packaging unit | 1 Pc |
| Item Nr. | Diameter | Holder | |
| WS-D22.00 RT19 | 3602200 | 22,00 |
WST-D22.0-3xD-H WST-D22.0-5xD-H WST-D22.0-8xD-H |
| WS-D22.10 RT19 | 3602210 | 22,10 | |
| WS-D22.20 RT19 | 3602220 | 22,20 | |
| WS-D22.23 RT19 | 3602223 | 22,23 | |
| WS-D22.30 RT19 | 3602230 | 22,30 | |
| WS-D22.40 RT19 | 3602240 | 22,40 | |
| WS-D22.50 RT19 | 3602250 | 22,50 | |
| WS-D22.60 RT19 | 3602260 | 22,60 | |
| WS-D22.62 RT19 | 3602262 | 22,62 | |
| WS-D22.70 RT19 | 3602270 | 22,70 | |
| WS-D22.80 RT19 | 3602280 | 22,80 | |
| WS-D22.90 RT19 | 3602290 | 22,90 |
The WS RT19 interchangeable drill tips in the diameter range of 22.00 to 22.90 mm are designed for professional drilling applications. They provide a solid foundation for machining steel and cast iron, helping to reduce setup times through an efficient interchangeable tip system.
Please pay attention to the holder/drill bit combinations!
These drill bits only fit the WST D22.0-..xD-H holder (22.00 to 22.90 mm).
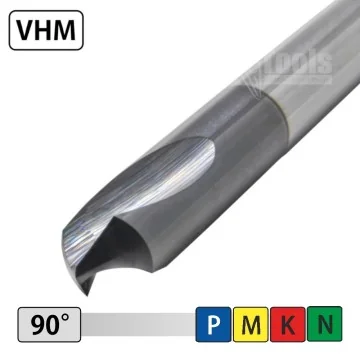
| Tool | Solid Carbide Spotting Drill 90° |
| Material | Steel, Stainless Steel, Cast Iron, NF-Materials |
| Shank | Cylindrical Shank |
| Packaging unit | 1 Pc |
| d1 | d2 | L1 | L2 | |
| AB-90°-D3.0 RT303 | 3 | 3 | 46 | 10 |
| AB-90°-D4.0 RT303 | 4 | 4 | 62 | 10 |
| AB-90°-D5.0 RT303 | 5 | 5 | 62 | 10 |
| AB-90°-D6.0 RT303 | 6 | 6 | 66 | 15 |
| AB-90°-D8.0 RT303 | 8 | 8 | 79 | 17 |
| AB-90°-D10.0 RT303 | 10 | 10 | 89 | 20 |
| AB-90°-D12.0 RT303 | 12 | 12 | 102 | 25 |
| AB-90°-D14.0 RT303 | 14 | 14 | 107 | 30 |
| AB-90°-D16.0 RT303 | 16 | 16 | 115 | 35 |
| AB-90°-D20.0 RT303 | 20 | 20 | 131 | 40 |
The solid carbide spotting drill 90° in grade RT303 is specifically designed for exact positioning and centering tasks. Featuring a cylindrical shank and a proven TiAlN coating, it provides an excellent foundation for reliable machining across various materials. This tool supports efficient workflows in metal cutting and ensures accurate guidance for subsequent drilling operations.
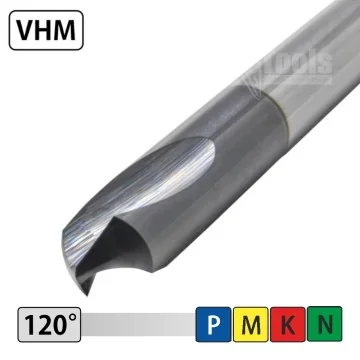
| Tool | Solid Carbide Spotting Drill 120° |
| Material | Steel, Stainless Steel, Cast Iron, NF-Materials |
| Shank | Cylindrical Shank |
| Packaging unit | 1 Pc |
| d1 | d2 | L1 | L2 | |
| AB-120°-D3.0 RT303 | 3 | 3 | 46 | 10 |
| AB-120°-D4.0 RT303 | 4 | 4 | 62 | 10 |
| AB-120°-D5.0 RT303 | 5 | 5 | 62 | 10 |
| AB-120°-D6.0 RT303 | 6 | 6 | 66 | 15 |
| AB-120°-D8.0 RT303 | 8 | 8 | 79 | 17 |
| AB-120°-D10.0 RT303 | 10 | 10 | 89 | 20 |
| AB-120°-D12.0 RT303 | 12 | 12 | 102 | 25 |
| AB-120°-D14.0 RT303 | 14 | 14 | 107 | 30 |
| AB-120°-D16.0 RT303 | 16 | 16 | 115 | 35 |
| AB-120°-D20.0 RT303 | 20 | 20 | 131 | 40 |
The solid carbide spotting drill RT303 is an excellent choice for exact positioning and centering before the actual drilling operation. Featuring a 120° point angle, it optimally prepares the workpiece for subsequent drills, preventing tool wandering and significantly increasing process reliability. The highly resistant TiAlN coating and the universal cylindrical shank support efficient workflows in professional machining environments.

| Tool | Interchangeable tip drill |
| Diameter | For Inserts 22,00-22,90 mm |
| Types | 3xD/5xD/8xD |
| Packaging unit | 1 Pc |
| Drill Lenght | Diameter | D2 | L2 | D3 | L1 | L3 | |
| WST D22.0-3xD-H | 3xD | 22,00 - 22,90 mm | 25 | 56 | 32 | 69,0 | 153,4 |
| WST D22.0-5xD-H | 5xD | 22,00 - 22,90 mm | 25 | 56 | 32 | 115,0 | 198,4 |
| WST D22.0-8xD-H | 8xD | 22,00 - 22,90 mm | 25 | 56 | 32 | 184,0 | 265,9 |
The WST interchangeable tip drill serves as a robust base for precision drilling applications and offers reliable performance in professional machining operations. Please pay attention to the Holder/drill bit combinations! Only drill bits with a diameter of 22,00-22,90 mm fit on these supports.

| Tools | Inserts for interchangeable tip drills |
| Point Angle | 140° |
| Scope of Application | Steel and Cast Iron |
| Coating | RT19: CVD Coated P25/K20 Carbide Grade for universal drilling of steel and cast materials. |
| Packaging unit | 1 Pc |
| Item Nr. | Diameter | Holder | |
| WS-D24.00 RT19 | 3602400 | 24,00 |
WST-D24.0-3xD-H WST-D24.0-5xD-H WST-D24.0-8xD-H |
| WS-D24.10 RT19 | 3602410 | 24,10 | |
| WS-D24.20 RT19 | 3602420 | 24,20 | |
| WS-D24.21 RT19 | 3602421 | 24,21 | |
| WS-D24.30 RT19 | 3602430 | 24,30 | |
| WS-D24.40 RT19 | 3602440 | 24,40 | |
| WS-D24.50 RT19 | 3602450 | 24,50 | |
| WS-D24.60 RT19 | 3602460 | 24,60 | |
| WS-D24.61 RT19 | 3602461 | 24,61 | |
| WS-D24.70 RT19 | 3602470 | 24,70 | |
| WS-D24.80 RT19 | 3602480 | 24,80 | |
| WS-D24.90 RT19 | 3602490 | 24,90 |
The WS RT19 series solid carbide interchangeable drill tips offer a reliable solution for professional drilling applications. Designed specifically for machining steel and cast iron, they provide precise cutting performance. Please pay attention to the holder/drill bit combinations! These drill bits only fit the WST D24.0-..xD-H holder (24.00 to 24.90 mm).

| Tools | Inserts for interchangeable tip drills |
| Point Angle | 140° |
| Scope of Application | Steel and Cast Iron |
| Coating | RT19: CVD Coated P25/K20 Carbide Grade for universal drilling of steel and cast materials. |
| Packaging unit | 1 Pc |
| Item Nr. | Diameter | Holder | |
| WS-D25.00 RT19 | 3602500 | 25,00 |
WST-D25.0-3xD-H WST-D25.0-5xD-H WST-D25.0-8xD-H |
| WS-D25.10 RT19 | 3602510 | 25,10 | |
| WS-D25.20 RT19 | 3602520 | 25,20 | |
| WS-D25.30 RT19 | 3602530 | 25,30 | |
| WS-D25.40 RT19 | 3602540 | 25,40 | |
| WS-D25.50 RT19 | 3602550 | 25,50 | |
| WS-D25.60 RT19 | 3602560 | 25,60 | |
| WS-D25.67 RT19 | 3602567 | 25,67 | |
| WS-D25.70 RT19 | 3602570 | 25,70 | |
| WS-D25.80 RT19 | 3602580 | 25,80 | |
| WS-D25.90 RT19 | 3602590 | 25,90 |
The WS RT19 solid carbide interchangeable drill tips (25.00 to 25.90 mm) are a well-thought-out solution for professional drilling tasks in steel and cast iron. Please pay attention to the holder/drill bit combinations! These drill bits only fit the WST D25.0-..xD-H holder (25.00 to 25.90 mm).

| Tools | Inserts for interchangeable tip drills |
| Point Angle | 140° |
| Scope of Application | Steel and Cast Iron |
| Coating | RT19: CVD Coated P25/K20 Carbide Grade for universal drilling of steel and cast materials. |
| Packaging unit | 1 Pc |
| Item Nr. | Diameter | Holder | |
| WS-D13.50 RT19 | 3601350 | 13,50 |
WST-D13.5-3xD-H WST-D13.5-5xD-H WST-D13.5-8xD-H |
| WS-D13.60 RT19 | 3601360 | 13,60 | |
| WS-D13.70 RT19 | 3601370 | 13,70 | |
| WS-D13.80 RT19 | 3601380 | 13,80 | |
| WS-D13.89 RT19 | 3601389 | 13,89 | |
| WS-D13.90 RT19 | 3601390 | 13,90 |
The WS RT19 solid carbide interchangeable drill tips in the diameter range from 13.50 to 13.90 mm are designed for universal drilling of steel and cast iron. When combined with the appropriate WST D13.5 holders, this system supports efficient workflows with long tool life and reliable chip evacuation. Please pay attention to the carrier/drill bit combinations: These drill bits only fit the 13.50-13.90 mm WST D13.5 carrier.

| Tools | Inserts for interchangeable tip drills |
| Point Angle | 140° |
| Scope of Application | Steel and Cast Iron |
| Coating | RT19: CVD Coated P25/K20 Carbide Grade for universal drilling of steel and cast materials. |
| Packaging unit | 1 Pc |
| Art. Nr. | Durchmesser | Träger | |
| WS-D19.00 RT19 | 3601900 | 19,00 |
WST-D19.0-3xD-H WST-D19.0-5xD-H WST-D19.0-8xD-H |
| WS-D19.05 RT19 | 3601905 | 19,05 | |
| WS-D19.10 RT19 | 3601910 | 19,10 | |
| WS-D19.20 RT19 | 3601920 | 19,20 | |
| WS-D19.27 RT19 | 3601927 | 19,27 | |
| WS-D19.30 RT19 | 3601930 | 19,30 | |
| WS-D19.40 RT19 | 3601940 | 19,40 | |
| WS-D19.45 RT19 | 3601945 | 19,45 | |
| WS-D19.50 RT19 | 3601950 | 19,50 | |
| WS-D19.60 RT19 | 3601960 | 19,60 | |
| WS-D19.70 RT19 | 3601970 | 19,70 | |
| WS-D19.80 RT19 | 3601980 | 19,80 | |
| WS-D19.84 RT19 | 3601984 | 19,84 | |
| WS-D19.90 RT19 | 3601990 | 19,90 |
The solid carbide drill insert WS RT19 (diameter range 19.00 to 19.90 mm) is engineered for professional drilling operations in steel and cast iron. Featuring a highly wear-resistant CVD coating and the robust P25/K20 carbide grade, this drill tip ensures reliable performance in universal machining tasks. Please pay attention to the carrier/drill bit combinations! These drill bits only fit the 19.00-19.90 mm carrier.

| Tools | Inserts for interchangeable tip drills |
| Point Angle | 140° |
| Scope of Application | Steel and Cast Iron |
| Coating | RT19: CVD Coated P25/K20 Carbide Grade for universal drilling of steel and cast materials. |
| Packaging unit | 1 Pc |
| Art. Nr. | Diameter | Holder | |
| WS-D10.50 RT19 | 3601050 | 10,50 |
WST-D10.5-3xD-H WST-D10.5-5xD-H WST-D10.5-8xD-H |
| WS-D10.60 RT19 | 3601060 | 10,60 | |
| WS-D10.70 RT19 | 3601070 | 10,70 | |
| WS-D10.72 RT19 | 3601072 | 10,72 | |
| WS-D10.80 RT19 | 3601080 | 10,80 | |
| WS-D10.90 RT19 | 3601090 | 10,90 |
The WS RT19 solid carbide interchangeable drill tips in the diameter range of 10.50 to 10.90 mm are designed for powerful and reliable drilling operations in steel and cast iron. With their precise interface for the matching carriers, the cutting edge can be changed directly in the machine, effectively minimizing setup times.
Please pay attention to the carrier/drill bit combinations!
These drill bits only fit the 10,50-10,90 mm carrier

| Tools | Inserts for interchangeable tip drills |
| Point Angle | 140° |
| Scope of Application | Steel and Cast Iron |
| Coating | RT19: CVD Coated P25/K20 Carbide Grade for universal drilling of steel and cast materials. |
| Packaging unit | 1 Pc |
| Item Nr. | Diameter | Holder | |
| WS-D27.00 RT19 | 3602700 | 27,00 |
WST-D27.0-3xD-H WST-D27.0-5xD-H WST-D27.0-8xD-H |
| WS-D27.38 RT19 | 3602738 | 27,38 | |
| WS-D27.50 RT19 | 3602750 | 27,50 | |
| WS-D27.78 RT19 | 3602778 | 27,78 |
The WS... RT19 solid carbide interchangeable drill tip in the diameter range from 27,00 to 27,78 mm is designed for high-performance and reliable drilling in steel and cast iron. The precise interface allows for a quick tool change directly in the machine, effectively minimizing setup times. Please pay attention to the holder/drill bit combinations!
These drill bits only fit the WST D27.0-..xD-H holder (27,00 to 27,78 mm).

| Tools | Inserts for interchangeable tip drills |
| Point Angle | 140° |
| Scope of Application | Steel and Cast Iron |
| Coating | RT19: CVD Coated P25/K20 Carbide Grade for universal drilling of steel and cast materials. |
| Packaging unit | 1 Pc |
| Art. Nr. | Diameter | Holder | |
| WS-D11.50 RT19 | 3601150 | 11,50 |
WST-D11.5-3xD-H WST-D11.5-5xD-H WST-D11.5-8xD-H |
| WS-D11.51 RT19 | 3601151 | 11,51 | |
| WS-D11.60 RT19 | 3601160 | 11,60 | |
| WS-D11.70 RT19 | 3601170 | 11,70 | |
| WS-D11.80 RT19 | 3601180 | 11,80 | |
| WS-D11.90 RT19 | 3601190 | 11,90 | |
| WS-D11.91 RT19 | 3601191 | 11,91 |
The WS RT19 solid carbide drill tips, available in diameters from 11.50 to 11.91 mm, provide a reliable solution for universal drilling applications. Please pay attention to the carrier/drill bit combinations! These drill bits only fit the WST D11.5-..xD-H carrier.

| Tools | Inserts for interchangeable tip drills |
| Point Angle | 140° |
| Scope of Application | Steel and Cast Iron |
| Coating | RT19: CVD Coated P25/K20 Carbide Grade for universal drilling of steel and cast materials. |
| Packaging unit | 1 Pc |
| Item Nr. | Diameter | Holder | |
| WS-D26.00 RT19 | 3602600 | 26,00 |
WST-D26.0-3xD-H WST-D26.0-5xD-H WST-D26.0-8xD-H |
| WS-D26.19 RT19 | 3602619 | 26,19 | |
| WS-D26.50 RT19 | 3602650 | 26,50 | |
| WS-D26.59 RT19 | 3602659 | 26,59 | |
| WS-D26.99 RT19 | 3602699 | 26,99 |
The WS... RT19 interchangeable tips offer high-performance drilling in the diameter range of 26.00 to 26.99 mm. They are designed for productive machining in industrial applications.
Please pay attention to the holder/drill bit combinations!
These drill bits only fit the WST D26.0-..xD-H holder (26.00 to 26.99 mm).

| Tools | Inserts for interchangeable tip drills |
| Point Angle | 140° |
| Scope of Application | Steel and Cast Iron |
| Coating | RT19: CVD Coated P25/K20 Carbide Grade for universal drilling of steel and cast materials. |
| Packaging unit | 1 Pc |
| Item Nr. | Diameter | Holder | |
| WS-D31.00 RT19 | 3603100 | 31,00 |
WST-D31.0-3xD-H WST-D31.0-5xD-H WST-D31.0-8xD-H |
| WS-D31.35 RT19 | 3603135 | 31,35 | |
| WS-D31.50 RT19 | 3603150 | 31,50 | |
| WS-D31.75 RT19 | 3603175 | 31,75 |
The WS RT19 interchangeable drill tip is designed for reliable drilling operations in steel and cast iron. When combined with the appropriate WST holder, this cutting insert creates favorable conditions for efficient machining processes.
Please pay attention to the holder/drill bit combinations!
These drill bits only fit the WST D31.0-..xD-H holder (31.00 to 31.75 mm).

| Tools | Inserts for interchangeable tip drills |
| Point Angle | 140° |
| Scope of Application | Steel and Cast Iron |
| Coating | RT19: CVD Coated P25/K20 Carbide Grade for universal drilling of steel and cast materials. |
| Packaging unit | 1 Pc |
| Item Nr. | Diameter | Holder | |
| WS-D28.00 RT19 | 3602800 | 28,00 |
WST-D28.0-3xD-H WST-D28.0-5xD-H WST-D28.0-8xD-H |
| WS-D28.18 RT19 | 3602818 | 28,18 | |
| WS-D28.50 RT19 | 3602850 | 28,50 | |
| WS-D28.58 RT19 | 3602858 | 28,58 | |
| WS-D28.97 RT19 | 3602897 | 28,97 |
The CVD-coated solid carbide interchangeable drill tip of the WS RT19 series, available in diameters from 28.00 to 28.97 mm, is designed for reliable drilling operations in steel and cast iron. When combined with the appropriate WST holders, it ensures high tool life and fast tip changes directly on the machine.
Please pay attention to the holder/drill bit combinations!
These drill bits only fit the WST D28.0-..xD-H holder (28,00 to 28,97 mm).

| Tools | Inserts for interchangeable tip drills |
| Point Angle | 140° |
| Scope of Application | Steel and Cast Iron |
| Coating | RT19: CVD Coated P25/K20 Carbide Grade for universal drilling of steel and cast materials. |
| Packaging unit | 1 Pc |
| Item Nr. | Diameter | Holder | |
| WS-D16.00 RT19 |
3601600 | 16,00 |
WST-D16.0-3xD-H WST-D16.0-5xD-H WST-D16.0-8xD-H |
| WS-D16.09 RT19 |
3601609 | 16,09 | |
| WS-D16.10 RT19 |
3601610 | 16,10 | |
| WS-D16.20 RT19 | 3601620 | 16,20 | |
| WS-D16.27 RT19 |
3601627 | 16,27 | |
| WS-D16.30 RT19 | 3601630 | 16,30 | |
| WS-D16.40 RT19 | 3601640 | 16,40 | |
| WS-D16.50 RT19 | 3601650 | 16,50 | |
| WS-D16.60 RT19 | 3601660 | 16,60 | |
| WS-D16.67 RT19 | 3601667 | 16,67 | |
| WS-D16.70 RT19 | 3601670 | 16,70 | |
| WS-D16.80 RT19 | 3601680 | 16,80 | |
| WS-D16.90 RT19 | 3601690 | 16,90 |
The solid carbide interchangeable drill tips WS RT19 are designed for demanding drilling tasks. Featuring a CVD-coated P25/K20 carbide grade and a 140° point angle, they provide a reliable solution for machining steel and cast materials. Please pay attention to the carrier/drill bit combinations! These drill bits only fit the 16,00-16,90 mm carrier.

| Tools | Inserts for interchangeable tip drills |
| Point Angle | 140° |
| Scope of Application | Steel and Cast Iron |
| Coating | RT19: CVD Coated P25/K20 Carbide Grade for universal drilling of steel and cast materials. |
| Packaging unit | 1 Pc |
| Art. Nr. | Diameter | Holder | |
| WS-D10.00 RT19 |
3601000 | 10,00 |
WST-D10.0-3xD-H WST-D10.0-5xD-H WST-D10.0-8xD-H |
| WS-D10.10 RT19 |
3601010 | 10,10 | |
| WS-D10.20 RT19 |
3601020 | 10,20 | |
| WS-D10.30 RT19 |
3601030 | 10,30 | |
| WS-D10.32 RT19 |
3601032 | 10,32 | |
| WS-D10.40 RT19 | 3601040 | 10,40 |
The WS... RT19 interchangeable drill tips (10.00 to 10.40 mm) are high-performance inserts designed specifically for drilling steel and cast iron. Featuring a CVD-coated P25/K20 carbide grade, they provide a well-thought-out solution for stable processes and clean drilling results in industrial applications. Please pay attention to the carrier/drill bit combinations! These drill bits only fit the 10.00-10.40 mm carrier.

| Tools | Inserts for interchangeable tip drills |
| Point Angle | 140° |
| Scope of Application | Steel and Cast Iron |
| Coating | RT19: CVD Coated P25/K20 Carbide Grade for universal drilling of steel and cast materials. |
| Packaging unit | 1 Pc |
| Item Nr. | Diameter | Holder | |
| WS-D23.00 RT19 | 3602300 | 23,00 |
WST-D23.0-3xD-H WST-D23.0-5xD-H WST-D23.0-8xD-H |
| WS-D23.02 RT19 | 3602302 | 23,02 | |
| WS-D23.10 RT19 | 3602310 | 23,10 | |
| WS-D23.20 RT19 | 3602320 | 23,20 | |
| WS-D23.30 RT19 | 3602330 | 23,30 | |
| WS-D23.40 RT19 | 3602340 | 23,40 | |
| WS-D23.42 RT19 | 3602342 | 23,42 | |
| WS-D23.50 RT19 | 3602350 | 23,50 | |
| WS-D23.60 RT19 | 3602360 | 23,60 | |
| WS-D23.70 RT19 | 3602370 | 23,70 | |
| WS-D23.80 RT19 | 3602380 | 23,80 | |
| WS-D23.81 RT19 | 3602381 | 23,81 | |
| WS-D23.90 RT19 | 3602390 | 23,90 |
The WS RT19 interchangeable drill tips in the diameter range of 23.00 to 23.90 mm offer a sophisticated solution for professional drilling applications. They are specially designed for use with WST D23.0-..xD-H holders and create good conditions for efficient workflows when machining steel and cast materials. Please pay attention to the holder/drill bit combinations! These drill bits only fit the WST D23.0-..xD-H holder (23.00 to 23.90 mm).

| Tools | Inserts for interchangeable tip drills |
| Point Angle | 140° |
| Scope of Application | Steel and Cast Iron |
| Coating | RT19: CVD Coated P25/K20 Carbide Grade for universal drilling of steel and cast materials. |
| Packaging unit | 1 Pc |
| Item Nr. | Diameter | Holder | |
| WS-D15.50 RT19 | 3601550 | 15,50 |
WST-D15.5-3xD-H WST-D15.5-5xD-H WST-D15.5-8xD-H |
| WS-D15.60 RT19 | 3601560 | 15,60 | |
| WS-D15.70 RT19 | 3601570 | 15,70 | |
| WS-D15.80 RT19 | 3601580 | 15,80 | |
| WS-D15.88 RT19 | 3601588 | 15,88 | |
| WS-D15.90 RT19 | 3601590 | 15,90 |
The WS RT19 solid carbide interchangeable tip is designed for precise drilling in steel and cast iron. When used with the appropriate WST drill body, this tool supports efficient workflows and enables quick tip changes directly in the machine.
Please pay attention to the carrier/drill bit combinations! These drill bits only fit the 15,50-15,90 mm carrier.

| Tools | Inserts for interchangeable tip drills |
| Point Angle | 140° |
| Scope of Application | Steel and Cast Iron |
| Coating | RT19: CVD Coated P25/K20 Carbide Grade for universal drilling of steel and cast materials. |
| Packaging unit | 1 Pc |
| Item Nr. | Diameter | Holder | |
| WS-D21.00 RT19 | 3602100 | 21,00 |
WST-D21.0-3xD-H WST-D21.0-5xD-H WST-D21.0-8xD-H |
| WS-D21.03 RT19 | 3602103 | 21,03 | |
| WS-D21.10 RT19 | 3602110 | 21,10 | |
| WS-D21.20 RT19 | 3602120 | 21,20 | |
| WS-D21.30 RT19 | 3602130 | 21,30 | |
| WS-D21.40 RT19 | 3602140 | 21,40 | |
| WS-D21.43 RT19 | 3602143 | 21,43 | |
| WS-D21.50 RT19 | 3602150 | 21,50 | |
| WS-D21.60 RT19 | 3602160 | 21,60 | |
| WS-D21.70 RT19 | 3602170 | 21,70 | |
| WS-D21.80 RT19 | 3602180 | 21,80 | |
| WS-D21.83 RT19 | 3602183 | 21,83 | |
| WS-D21.90 RT19 | 3602190 | 21,90 |
The CVD-coated interchangeable drill tips WS... RT19 in the 21.00 to 21.90 mm range are designed for professional applications. They provide a versatile solution for machining steel and cast iron materials.
Please pay attention to the holder/drill bit combinations!
These drill bits only fit the WST D21.0-..xD-H holder (21.00 to 21.90 mm).

| Tools | Inserts for interchangeable tip drills |
| Point Angle | 140° |
| Scope of Application | Steel and Cast Iron |
| Coating | RT19: CVD Coated P25/K20 Carbide Grade for universal drilling of steel and cast materials. |
| Packaging unit | 1 Pc |
| Item Nr. | Diameter | Holder | |
| WS-D12.00 RT19 |
3601200 | 12,00 |
WST-D12.0-3xD-H WST-D12.0-5xD-H WST-D12.0-8xD-H |
| WS-D12.10 RT19 |
3601210 | 12,10 | |
| WS-D12.20 RT19 |
3601220 | 12,20 | |
| WS-D12.30 RT19 |
3601230 | 12,30 | |
| WS-D12.40 RT19 | 3601240 | 12,40 |
The WS... RT19 solid carbide interchangeable drill tips (12.00 - 12.40 mm) are designed for universal drilling operations in steel and cast iron. Featuring a high-performance CVD coating, these inserts provide excellent wear resistance. They are precisely matched to the WST D12.0-..xD-H carriers, supporting efficient and stable processes in professional metalworking applications.